



Pin Punch untuk Blanking Halus: Izin, Selesai, dan Kualitas Tepi
Punch pins for fine blanking cannot be selected by hardness, pelapisan, or nominal diameter alone. Edge quality depends on how the punch works with the die, blankholder, V-ring, counterpunch, work material, pelumasan, and press alignment. Very small clearance makes the process especially sensitive to profile error, keausan tepi, kerusakan permukaan, and side loading.
This guide focuses on those fineblanking-specific requirements. Untuk informasi lebih luas tentang tipe die, bahan perkakas, and general purchasing considerations, lihat Panduan Cetakan Meninju (disimpulkan).
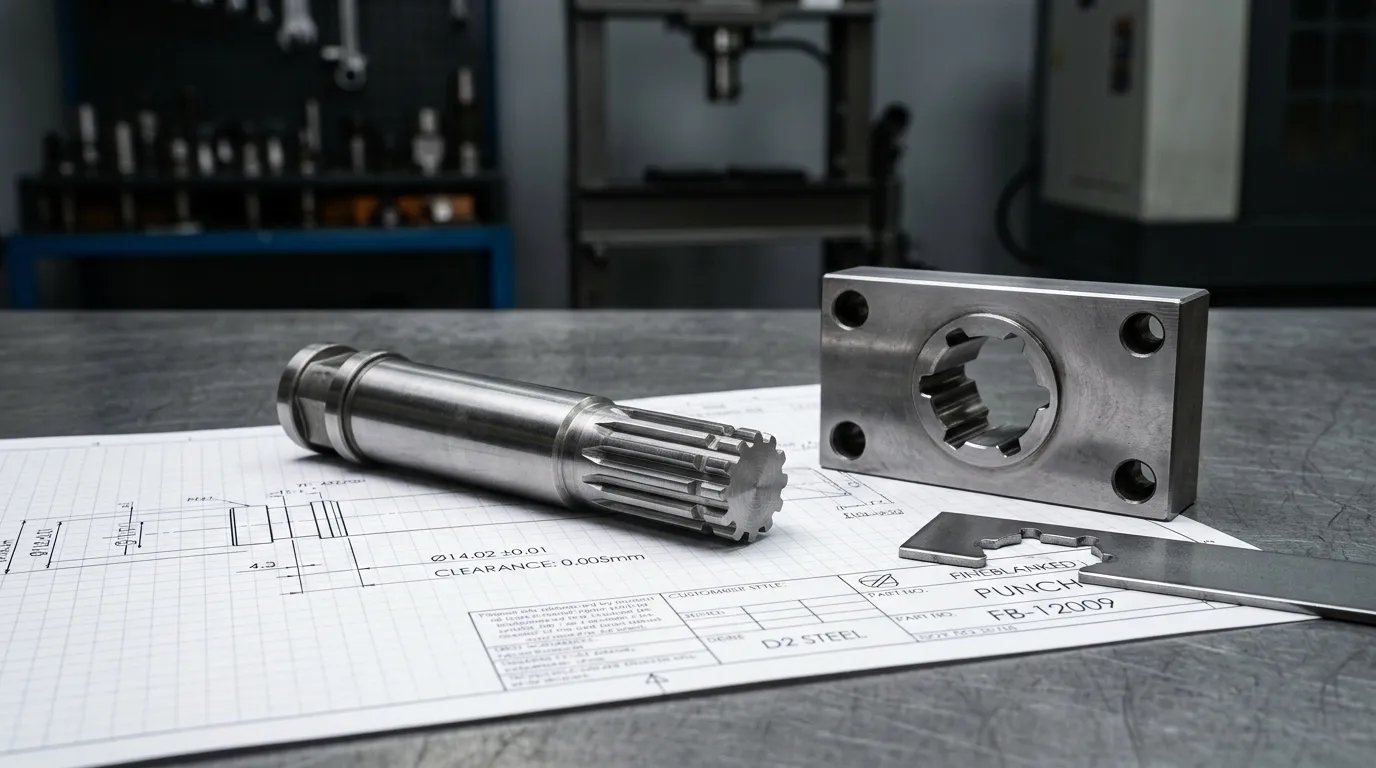
Mengapa Pukulan Fineblanking Membutuhkan Spesifikasi Tingkat Sistem
Fineblanking produces a high proportion of controlled shear by restraining the sheet before and during cutting. The blankholder clamps the material, a V-ring or impingement ring limits lateral flow, and the counterpunch applies pressure from the opposite side. The punch and die then separate the material through a very small clearance.
This system changes the stress state around the cutting line. It can reduce the fracture zone and improve edge perpendicularity compared with conventional blanking, but it also makes tooling errors more visible. A punch that is dimensionally correct on its own may still perform poorly if the guide fit, die position, counterpressure, or material condition creates uneven local clearance.
A Studi Fineblanking yang ditinjau oleh rekan sejawat describes the interaction among clearance, V-ring geometry, counterpressure, cutting-edge preparation, dan aliran material. This relationship is why a fineblanking punch should be specified as one part of a matched system.
Distinguish the Blanking Punch, Piercing Punch, and Generic Punch Pin
“Punch pin” is a broad product term. In a fineblanking application, the drawing should identify the actual cutting function.
| Istilah perkakas | Fungsi | Dimensi yang biasa dikendalikan |
|---|---|---|
| Pukulan pengosongan | Memotong profil eksternal dari bagian yang dipertahankan | Bekerja dengan bukaan cetakan yang mengontrol ukuran kosong yang sudah jadi |
| Pukulan menusuk | Menghasilkan lubang atau bukaan internal | Biasanya mengontrol ukuran lubang jadi |
| Pin punch | Istilah umum yang dapat menggambarkan salah satu fungsi | Harus diklarifikasi pada gambar atau RFQ |
This distinction matters because the punch and die are not dimensioned or edge-prepared in the same way for external blanking and internal piercing.
Using only “punch pin” on an RFQ leaves several questions unanswered:
- Is the finished feature an external blank or an internal hole?
- Which member controls the finished dimension?
- Which cutting edge must remain sharp?
- Where is the intended radius or edge preparation?
- Is the punch guided through a plate?
- How is clearance defined?
These details affect the punch profile, Pembukaan, inspection method, and regrinding plan.
Cocokkan persiapan mutakhir dengan blanking atau piercing
For standard external fineblanking, the punch cutting edge is generally kept sharp while the corresponding die edge is prepared with a controlled radius. Dalam tindik, the relationship is reversed: the piercing punch receives the relevant edge preparation while the die edge remains sharp.
This blanking-versus-piercing distinction is supported by fineblanking research and should be shown explicitly on the tool drawing. It should not be left to a generic note such as “break all sharp edges.”
Uncontrolled polishing can be just as harmful as an incorrect radius. Polishing the cutting edge may:
- Round an edge that should remain sharp.
- Change the effective punch profile.
- Increase local clearance.
- Produce inconsistent edge preparation around corners.
- Remove a coating from a critical area.
- Hide grinding damage without correcting the underlying geometry.
Edge preparation should therefore be specified by location and function. The punch face, flank, guide surface, and cutting edge do not necessarily require the same treatment.
Set Clearance by Material, Geometri, and Edge Requirement
Fineblanking uses much smaller punch–die clearance than conventional blanking. Small clearance supports a larger clean-shear zone, but it also increases cutting force, gesekan, panas, and sensitivity to alignment.
Some technical literature cites clearance around 0.5% of sheet thickness as a basic fineblanking guideline. The same research warns that this value must be adapted to the geometry and application. It is a starting point for engineering evaluation, not a universal production specification.
The final clearance decision should account for:
- Material grade and condition.
- Sheet thickness and thickness tolerance.
- Kekerasan, kekuatan tarik, and ductility.
- Microstructure and rolling direction.
- Part profile and corner geometry.
- Required clean-shear depth.
- Allowed fracture zone and burr height.
- V-ring and counterpunch forces.
- Punch and die rigidity.
- Pelumasan.
- Tool material and cutting-edge condition.
- Expected wear during the production run.
Clearance should be validated against the assembled tool and actual work material. A punch supplier cannot establish finished edge quality from the punch drawing alone if the die, sistem panduan, force settings, and material condition are unknown.
Specify Per-Side, Total, and Relative Clearance Correctly
A drawing should state whether the listed clearance is per side or total.
For a symmetrical profile:
- Pembersihan per sisi, c: gap between the punch and die on one side.
- Total clearance: combined clearance across both sides, normally 2c.
- Relative clearance: per-side or total clearance expressed as a percentage of sheet thickness. The convention must be stated.
Misalnya, if the per-side clearance is shown as 0.01 mm, the total diametral difference between a round punch and die opening is 0.02 mm. This is only a dimensional illustration, not a recommended fineblanking value.
The controlling dimension also changes with the operation:
- In external blanking, the die opening normally controls the retained blank profile. The punch is smaller by the total clearance.
- Dalam tindik, the punch normally controls the hole profile. The die opening is larger by the total clearance.
A complete drawing should identify:
- Whether the operation is blanking or piercing.
- The finished feature dimension.
- The punch dimension.
- The die dimension.
- Whether clearance is per side or total.
- The relevant datums and geometric tolerances.
Without these details, two suppliers may interpret the same clearance note differently.
Diagnose Clearance That Is Too Small, Too Large, or Uneven
| Kondisi izin bebas | Kemungkinan efek tepi atau perkakas | Memeriksa sebelum mengubah nilai nominal |
| Terlalu besar | Earlier fracture, wider fracture zone, increased taper, larger burr, reduced clean shear | Punch and die wear, material thickness, kondisi tepi, actual assembled dimensions |
| Terlalu kecil | Higher cutting load, panas, gesekan, menyebalkan, accelerated wear, chipping sensitivity | Force settings, pelumasan, penyelarasan, punch toughness, corner geometry |
| Tidak merata di sekitar profil | One-sided burr, local fracture, pemuatan samping, asymmetric wear, retak tepi | Punch straightness, Penyesuaian, kondisi panduan, fitting holder, profile accuracy |
Uneven clearance is often more damaging than a slightly imperfect nominal value. A drawing may specify the correct average gap while the assembled tool produces a smaller gap on one side and a larger gap on the other.
Penyebab yang mungkin meliputi:
- Punch straightness error.
- Worn guide plate or bushing.
- Incorrect shank or holder fit.
- Misaligned die inserts.
- Profile error after regrinding.
- Tekan atau mati-set defleksi.
- Material feeding at an angle.
- Local coating buildup or damage.
Itu Panduan Komponen Die provides broader context on guide systems, wear parts, and component alignment. In a fineblanking tool, those components directly influence the clearance that exists under load.
Tentukan hasil akhir dan geometri punch tanpa merusak ujung tombak
A single surface-roughness value does not fully define a fineblanking punch. The punch face, flank, terdepan, guide surface, batang, and transition features perform different functions.
The flank slides against the work material and may be exposed to pickup, penilaian, and adhesive wear. The guide surface controls positioning and side load. The cutting edge defines the start of material separation. A finish requirement should identify the exact surface and its purpose.
Average roughness, or Ra, is useful, but it can hide isolated deep scratches. Two surfaces with similar Ra values may behave differently if one contains directional grinding marks, torn material, pits, or high peak-to-valley variation.
Where the application is sensitive, the specification may also address:
- Rz, rt, or another peak-to-valley parameter.
- Measurement direction.
- Measurement location.
- Sampling length and cutoff.
- Maximum scratch depth.
- Visual or optical acceptance criteria.
- Grinding-burn inspection.
- EDM recast-layer removal.
- Coating condition at the cutting edge.
Control the Face, Sayap, Guide Surface, and Cutting Edge Separately
| Area pukulan | Fungsi utama | Risiko utama |
| Ujung tombak | Memulai dan mengontrol geser | Rounding, mengelupas, incorrect radius, coating buildup |
| Sayap | Meluncur melewati bahan kerja | Membelokkan, pengambilan, penilaian, keausan abrasif |
| Pukulan wajah | Mentransfer beban pemotongan | Terkelupas, deformasi, kerusakan penggilingan |
| Permukaan panduan | Mengontrol posisi dan beban samping | Excessive clearance, seizure, kontak tidak merata |
| Shank dan transisi | Hubungkan pukulan ke dudukan | Konsentrasi stres, poor fit, membengkokkan |
Polishing is useful only when it improves the intended surface without changing geometry. An operator should not polish across a critical edge or remove material until the surface “looks smooth.” The process should preserve profile size, kelurusan, kondisi tepi, dan fit.
Grinding direction also matters. Deep transverse marks on a sliding flank can increase resistance and create locations for material pickup. Fine longitudinal finishing may be more appropriate on a guided or sliding surface, provided it does not alter the punch dimensions.
Verify Profile Accuracy, Kelurusan, Konsentrisitas, and Runout
Very small nominal clearance requires accurate geometry throughout the punch assembly.
Akurasi profil controls local clearance around complex shapes. A small profile error near a corner can create excessive pressure even if the main dimensions are correct.
Kelurusan affects how the punch passes through the guide and enters the die. A long punch with slight bow may contact one side of the guide, producing side load and uneven clearance.
Konsentrisitas atau koaksialitas matters for round, berlangkah, or multi-diameter punches. It defines how one cylindrical feature relates to another datum axis.
Runout is a practical inspection result obtained during rotation. It can reveal eccentricity, surface error, or setup error, but it should not be treated as identical to concentricity.
The inspection plan should also account for:
- Diameter dan kesesuaian betis.
- Holder pocket condition.
- Guide-plate clearance.
- Punch protrusion and length.
- Die-insert location.
- Datum selection.
- Regrinding effects.
- Coating thickness on controlled surfaces.
A punch can meet its standalone dimensions and still produce poor results if the assembled tolerance stack shifts the cutting profile.
Pilih bahan pukulan dan lapisan dengan mode kegagalan dominan
The best punch material depends on how the tool is expected to fail. Hardness alone is not a sufficient selection criterion.
Relevant failure modes include:
- Abrasive wear from hard particles or abrasive stock.
- Keausan perekat dan galling.
- Chip tepi.
- Gross fracture.
- Deformasi plastik.
- Bending or side loading.
- Thermal damage.
- Delaminasi pelapis.
The work material, ketebalan, feature size, corner geometry, punch slenderness, kondisi panduan, pelumasan, and production volume all affect the choice.
Bandingkan baja dan karbida tanpa menyatakan pemenang universal
| Pilihan bahan | Potensi keuntungan | Batasan utama | Pertimbangan yang cocok |
| HSS atau baja perkakas | Ketangguhan, stabilitas tepi, easier regrinding, better tolerance of impact or slight misalignment | Dapat aus lebih cepat dalam aplikasi yang sangat abrasif | Geometri kompleks, pukulan ramping, applications with chipping or impact risk |
| Baja perkakas metalurgi serbuk | Ketahanan aus dan ketangguhan yang seimbang | Biaya yang lebih tinggi dan persyaratan perlakuan panas khusus material | Aplikasi yang membutuhkan ketahanan aus lebih tinggi daripada baja konvensional tanpa kerapuhan karbida penuh |
| Tungsten karbida | Kekuatan tekan tinggi dan ketahanan aus | Greater sensitivity to tensile stress, dampak, edge defects, dan ketidakselarasan | Rigid, well-guided applications dominated by abrasive wear |
Carbide is not automatically the best choice for every fineblanking punch. A highly wear-resistant carbide punch can chip quickly if the guide system introduces side loading or if a sharp internal corner concentrates stress. A tougher HSS or tool-steel punch may provide more stable service in that condition.
SunshinePro lists HSS grades and carbide among its general punch options. Readers comparing available products can review its pukulan baja berkecepatan tinggi dan Opsi pukulan karbida. The application still requires confirmation against the actual work material, geometri, pembersihan, dan mode kegagalan yang diharapkan.
Perlakukan Pelapis dan Pelumasan sebagai Kontrol Pendukung
SunshinePro mencantumkan TiN, TiCN, and DLC among coating options on relevant punch product pages. These coatings may change friction, adhesive-wear behavior, or abrasive-wear resistance, but they do not correct a poor base design.
A coating cannot fix:
- Excessive or uneven clearance.
- Incorrect edge preparation.
- A bent or misaligned punch.
- Ketangguhan substrat yang tidak memadai.
- Poor guide fit.
- Unsupported corner geometry.
- Insufficient lubrication.
- Grinding damage beneath the coating.
Coating thickness also matters when the clearance is extremely small. A coating applied to a controlled profile or guide surface may alter the final dimension if the drawing and grinding allowance do not account for it.
Coating selection should specify the substrate, kondisi perlakuan panas, coated surfaces, excluded surfaces, final dimensions, edge treatment, dan metode inspeksi.
Baca tepi halus untuk mendiagnosis masalah pukulan dan proses
The finished cut edge is a record of how the punch, Metode, work material, forces, pelumasan, and wear interacted during the stroke.
A fineblanked edge may contain:
- Die roll or rollover: rounded deformation near the entry side.
- Clean-shear or burnished zone: smoother area produced by controlled shearing.
- Zona patah: rougher area where material separation changes from shear to fracture.
- burr: projection at the exit side.
- Mengurangi: deviation from a perpendicular cut surface.
Itu Standar VDI 2906 Bagian 5 provides terminology and characteristic values for evaluating fineblanked cut faces. Formal acceptance criteria should be based on the applicable drawing and standard rather than an undefined requirement such as “smooth edge.”
Measure Die Roll, Clean Shear, Fraktur, burr, and Perpendicularity
Inspection should cover more than one cross-section. Edge quality can vary around corners, narrow webs, changes in profile direction, and areas affected by material rolling direction.
A practical inspection record may include:
- Posisi pengukuran.
- Material grade and lot.
- Ketebalan lembaran.
- Tool identification.
- Stroke count.
- Punch condition.
- Die-roll width or depth.
- Clean-shear depth.
- Fracture-zone depth.
- Burr height.
- Edge taper or perpendicularity.
- Photographs at controlled magnification.
Trend data is often more useful than a single measurement. A gradual increase in burr or fracture-zone depth may indicate progressive edge wear. A sudden one-sided defect is more likely to suggest chipping, ketidaksejajaran, guide damage, or material-positioning error.
Gunakan Matriks Defect-to-Cause-to-Check-to-Correction
| Kondisi yang diamati | Kemungkinan penyebab | Pemeriksaan | Koreksi arah |
| Zona fraktur menjadi lebih dalam | Kelebihan izin, worn edge, changed material condition, inadequate material restraint | Measure punch and die, inspect edge, verify material and force settings | Restore geometry, review clearance, confirm material and force conditions |
| Burr meningkat secara bertahap | Pembulatan tepi, keausan abrasif, Keausan | Compare against earlier parts, inspect edge under magnification | Giling ulang atau ganti perkakas yang terpengaruh setelah mengonfirmasi sisa tunjangan |
| Gerinda lebih besar di satu sisi | Clearance tidak merata, punch bow, pakaian panduan, die misalignment | Periksa kelurusan, guide contact, fitting holder, die position | Penyelarasan yang benar atau komponen yang aus sebelum mengubah jarak bebas nominal |
| Bahan menempel di sayap | Membelokkan, pelumasan yang tidak memadai, permukaan kasar, incompatible coating or substrate | Inspect pickup, menyelesaikan, lubrication delivery, suhu | Clean and restore surface, pelumasan yang benar, review material/coating system |
| Chiping tepi lokal | Brittle substrate, kelebihan beban, small clearance, dampak, beban samping, kerusakan penggilingan | Periksa lokasi patah tulang, penyelarasan, corner geometry, kondisi perlakuan panas | Hapus akar penyebab dan pilih keseimbangan ketangguhan/keausan yang sesuai |
| Profil selesai melayang | Memakai, deformasi, loose holder fit, guide damage, thermal change | Check punch profile, shank fit, pemandu, Metode, and measurement setup | Pulihkan komponen pengontrol dan validasi ulang izin |
These are investigation paths, not automatic diagnoses. Several conditions can create the same visible defect.
For broader analysis of fracture, membengkokkan, and fatigue-related failures, lihat kerusakan pukulan pada cetakan stamping.
Prepare the Drawing, Inspection Plan, and RFQ Before Ordering
A useful fineblanking punch inquiry needs more than a part number and nominal diameter. The supplier must understand the finished feature, work material, mating tool, quality target, dan metode inspeksi.
Sertakan data aplikasi yang mengontrol desain pukulan
Provide the following information where applicable:
- Finished-part drawing and critical dimensions.
- Identification of blanking or piercing.
- Work-material grade and condition.
- Sheet thickness and tolerance.
- Material hardness or tensile range.
- Coating or plated condition of the stock.
- Rolling direction when relevant.
- Required die roll, clean-shear depth, fracture limit, burr limit, and perpendicularity.
- Dimensi punch dan cetakan.
- Per-side or total clearance convention.
- Punch material and hardness requirement.
- Cutting-edge condition and specified radius.
- Flank and guide-surface finish.
- Kelurusan, konsentrisitas, coaxiality, and runout requirements.
- batang batang, pemegang, and guide interfaces.
- Coating type and coated surfaces.
- Regrinding allowance.
- Expected production environment.
- Existing defect photographs or samples when troubleshooting.
The RFQ should also identify which dimensions are final after coating and which surfaces must remain uncoated.
Request Evidence for Material, Kekerasan, Geometri, and Finish
Depending on the part risk and quality requirements, request appropriate documentation such as:
- Material certificate or traceability record.
- Catatan perlakuan panas.
- Hardness result and test method.
- Laporan inspeksi dimensi.
- Profile measurement.
- Straightness and runout results.
- Surface-roughness measurement, including location and direction.
- Cutting-edge visual or optical inspection.
- Coating specification and application record.
Some requirements can be verified on the loose punch. Others can only be validated after assembly with the die, sistem panduan, blankholder, and counterpunch.
The purchase specification should separate those two responsibilities clearly.
Cocokkan Kemampuan Terverifikasi SunshinePro dengan Spesifikasi Fineblanking
SunshinePro states that it supplies punching dies and pins and can manufacture non-standard mold accessories from customer drawings or samples. Its relevant product pages list HSS, tool-steel, and carbide options, along with processes such as CNC machining, penggilingan presisi, EDM on applicable products, and vacuum heat treatment on applicable punch products.
The company website also states general punch-and-pin capability of Ra 0.4 surface finish and dimensional tolerances within ±0.002 mm. These are general capability statements. They should not be treated as proof that the same values are suitable for every fineblanking application or that they guarantee a specific cut-edge result.
A technical inquiry should ask SunshinePro to confirm:
| Kemampuan umum terverifikasi | Detail aplikasi memerlukan konfirmasi |
| Manufaktur khusus dari gambar atau sampel | Apakah geometri blanking atau piercing yang diajukan layak |
| HSS, tool-steel, and carbide punch options | Substrat mana yang sesuai dengan risiko keausan dan keserpihan yang diharapkan |
| Penggilingan presisi dan proses EDM yang berlaku | How the final profile, tepi, and recast condition will be controlled |
| Pilihan pelapis yang dipilih | Coating suitability, thickness allowance, and coated surfaces |
| Kemampuan Ra Umum dan toleransi | Actual finish, profil, kelurusan, and inspection requirements for the application |
Prepare the finished-part drawing, work-material data, clearance definition, mating die information, edge-quality criteria, and inspection requirements before requesting a quotation. You can then Kirim spesifikasi pukulan untuk ditinjau and ask for confirmation of material, geometri, menyelesaikan, pelapisan, and inspection feasibility.
Bagikan:



Ditulis oleh Sunshine
di Sunshine, Kami adalah produsen dan pemasok profesional komponen cetakan presisi, menawarkan berbagai produk untuk aplikasi stamping dan cetakan injeksi. Fokus utama kami adalah mencetak cetakan, pin dan lengan ejector, serta tiang panduan dan bushing. Dengan pemesinan CNC canggih, kontrol kualitas ketat, dan kemampuan produksi yang kuat, kami memastikan keandalan, suku cadang presisi tinggi, bersama dengan komponen standar yang tersedia untuk pasokan global yang cepat dan efisien.
BERITA
DAPATKAN LAYANAN
Dengan suku cadang berkualitas untuk memenuhi setiap anggaran dan staf ramah yang terlatih untuk membuat kunjungan Anda menjadi informatif dan tanpa repot.
