



Toleransi Pin Pemosisian Cetakan untuk Penyelarasan yang Dapat Diulang
There is no single mold positioning pin tolerance that works for every mold. Repeatable alignment depends on a complete tolerance chain: the pin diameter, the mating hole or bushing diameter, the fit between them, the position and orientation of both features, and the dimensional changes that occur during operation.
A pin can be ground to a very tight diameter tolerance and still fail to locate the mold correctly if its hole is misplaced, its axis is tilted, or two locating pins create an overconstrained pattern. For broader guidance on guide systems, memakai, and fit selection, lihat pin cetakan dan bushing (disimpulkan). This guide focuses specifically on defining, calculating, documenting, and inspecting positioning-pin tolerances.
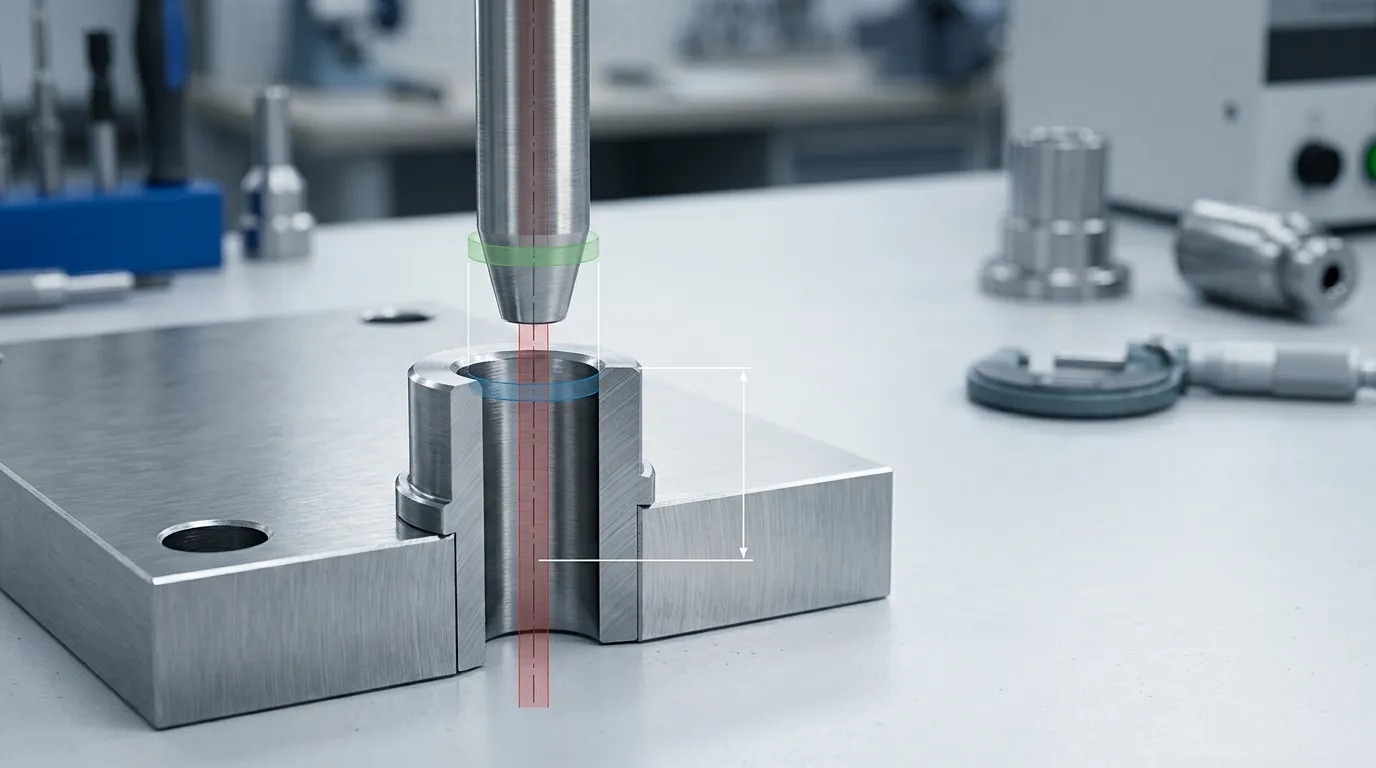
What Does a Mold Positioning Pin Tolerance Actually Control?
The word “tolerance” may refer to several different requirements. These controls are related, but they are not interchangeable.
| Kontrol | Apa yang Didefinisikan | Apa yang Tidak Didefinisikan |
|---|---|---|
| Toleransi ukuran pin | Diameter pin terbesar dan terkecil yang dapat diterima | Posisi sumbu pin |
| Toleransi lubang atau bushing | Lubang kawin terbesar dan terkecil yang dapat diterima | Apakah lubang ditempatkan dengan benar |
| Pas pin-ke-lubang | Kemungkinan jarak bebas atau gangguan antara kedua fitur tersebut | Kesalahan penyelarasan cetakan total |
| Toleransi geometris | Posisi dan orientasi sumbu pin atau lubang yang diizinkan | Jarak bebas aktual antara bagian-bagian |
| Pengulangan sistem | Seberapa konsisten cetakan kembali ke posisi yang sama | Apakah posisi berulang itu adalah posisi nominal yang benar |
Itu Sistem batas dan kesesuaian ISO 286-1 defines size tolerances and fit relationships for holes and shafts. It does not control where a hole is located or whether its axis is perpendicular to the mold plate. Those requirements need geometric controls, such as those defined by ISO 1101.
Size Tolerance, Cocok, and Alignment Are Different Requirements
Suppose a positioning pin and its mating hole are both within their specified diameter limits. That confirms only that their sizes are acceptable.
It does not confirm that:
- the pin and hole centers coincide;
- their axes are parallel;
- two locating holes have the correct spacing;
- the mold returns to its intended position;
- the assembly will still engage after heating or wear.
The actual fit comes from the combination of both size ranges. The smallest permitted hole paired with the largest permitted pin creates the tightest possible assembly. The largest hole paired with the smallest pin creates the loosest possible assembly.
Both extremes must be checked.
Posisi, Orientasi, and Repeatability Complete the Specification
A bore may have the correct diameter but still be offset from its basic location. A pin may be positioned correctly at the plate surface but tilted enough to bind over a long engagement length.
A complete positioning specification may therefore need:
- a functional datum reference frame;
- basic dimensions locating the pin or hole;
- positional tolerance;
- perpendicularity or another orientation control;
- pattern control for multiple locating features.
Repeatability and accuracy should also be distinguished. Repeatability describes how consistently the mold returns to the same position. Accuracy describes how close that position is to the intended nominal location.
A locating system can be repeatable but consistently offset if the feature pattern was manufactured in the wrong position.
Pin pemosisian tidak boleh secara otomatis diperlakukan setara dengan pin panduan cetakan. Guide pins primarily control movement as mold halves open and close. A dedicated positioning pin may establish a more precise final location after the mold halves approach engagement.
Tentukan persyaratan fungsional sebelum memilih kecocokan
A tolerance should start with the required function, not with a familiar fit designation.
Before assigning limits, mendefinisikan:
- The maximum permitted translational alignment error.
- The maximum permitted angular error.
- The nominal pin diameter and engagement length.
- Whether the pin is permanent, removable, or replaceable.
- How often the mold will be assembled or disassembled.
- Which side retains the pin.
- Which side provides the locating engagement.
- The operating temperature range.
- The expected wear, pelumasan, and contamination conditions.
- The manufacturing and inspection methods available.
- Whether binding or excess clearance creates the greater functional risk.
A positioning system used for a removable insert may prioritize easy engagement and interchangeability. A permanently installed locator may require stronger retention on its mounting side. A heated mold may need enough room for differential thermal expansion between the pin, bushing, and mold plate.
Application labels alone do not determine the correct fit. An “automotive mold” or “medical mold” still needs a defined alignment requirement, material combination, temperature range, dan rencana inspeksi.
Pisahkan Antarmuka Tetap dari Antarmuka Penempatan
The two ends of a positioning pin usually perform different jobs.
| Antarmuka | Fungsi Utama | Kemungkinan Arah Fit |
| Sisi pemasangan | Pertahankan pin di pelat pendukung dan pertahankan sumbunya | Controlled transition or interference, depending on design |
| Sisi lokasi | Masukkan lubang kawin atau bushing dan batasi gerakan relatif | Controlled clearance or transition, depending on function |
Using the same fit on both sides can create avoidable problems. A locating-side interference fit may prevent normal assembly. Excessive mounting-side clearance may allow the pin to shift or loosen.
The final selection must also consider plate thickness, surrounding material, removal method, replacement needs, and the risk of distortion during installation.
Pilih kecocokan dan hitung jarak bebas aktual
Izin, transition, and interference fits describe the relationship between the complete pin and hole tolerance zones.
Izin, Transisi, and Interference Serve Different Functions
| Jenis Fit | Hasil Dimensi | Penggunaan Fungsional Khas | Risiko Utama |
| Jarak bebas sesuai | Lubang terkecil tetap lebih besar dari pin terbesar | Keterlibatan penempatan geser atau yang dapat dilepas | Pergerakan berlebih jika jarak bebas terlalu besar |
| Transition fit | Some valid combinations have clearance; others have interference | Lokasi dekat atau retensi sedang | Gaya perakitan variabel |
| Interference fit | Pin terkecil tetap lebih besar dari lubang terbesar | Retensi permanen atau semi-permanen | Distorsi, difficult removal, or installation damage |
These categories describe outcomes, not universal recommendations. A clearance fit may be suitable on the locating side while an interference or transition fit is used on the mounting side.
The hole-basis system is common because standard hole-making tools can establish a defined hole tolerance while the shaft or pin tolerance is selected to create the required fit. Tetap saja, a designation such as H7/g6 or H7/m6 is incomplete without the nominal diameter and governing standard. The numerical deviations change across diameter ranges.
Gunakan Dimensi Batas untuk Memeriksa Kedua Ekstrem Perakitan
Calculate the limits before approving the fit.
Minimum clearance
Minimum clearance = Smallest permitted hole − Largest permitted pinMaximum clearance
Maximum clearance = Largest permitted hole − Smallest permitted pinA negative result represents interference.
Consider a hypothetical example:
| Fitur | Minimum Diameter | Diameter Maksimum |
| Menemukan lubang | 10.010 mm | 10.018 mm |
| Pin pemosisian | 9.998 milimeter | 10.004 mm |
The tightest possible assembly is:
10.010 − 10.004 = 0.006 mm minimum diametral clearanceThe loosest possible assembly is:
10.018 − 9.998 = 0.020 mm maximum diametral clearanceThese values are examples only. They are not recommended SunshinePro specifications or universal mold tolerances.
Diametral clearance also should not be treated as the complete alignment error. In an ideal single-pin interface, the pin center may move radially by up to approximately half the diametral clearance before contact. The actual mold position also depends on the second locator, feature positions, axis angles, engagement lengths, deformasi, dan kondisi operasional.
Control the Locating Pattern, Not Only the Pin Diameter
A precision fit cannot compensate for an incorrectly located pattern.
The pin and mating feature must be controlled from datums that represent how the mold is assembled and functions. These may include a seating face, a side reference, or another stable mold-base feature.
Use Functional Datums, Posisi, and Axis Control
A practical drawing should identify:
- the surfaces establishing the functional datum reference frame;
- the basic locations of the pin and mating hole;
- the permitted positional variation;
- any required perpendicularity or axis-orientation control;
- the relationship between multiple locating features.
ISO 5458 provides complementary rules for pattern specifications under the ISO GPS system. Drawings using ASME conventions should follow ASME Y14.5.
The drawing should clearly use one governing convention. Mixing ISO and ASME symbols or assumptions without clarification can create conflicting interpretations between the designer, manufacturer, and inspector.
Hindari Overconstraint dengan Pasangan Pin Bulat dan Lega
Two fully round pins entering two close-fitting round holes can overconstrain the assembly.
For both pins to engage, the distance between the pins must agree closely with the distance between the mating holes. Even when every individual diameter is acceptable, accumulated spacing and position variation can cause binding.
A common locating arrangement uses:
- one round pin as the primary locator;
- one diamond, relieved, or flattened pin as the secondary locator.
The round pin controls movement in two planar directions. The relieved pin controls the required secondary direction while allowing some variation along the relieved axis.
The secondary pin must be oriented correctly. Rotating its relieved direction by 90 degrees changes which movement it permits and which movement it controls.
Locator spacing also affects angular definition. Greater spacing can reduce angular movement for a given amount of linear clearance, but no universal spacing rule applies. Ukuran piring, loads, available space, hole-position capability, and engagement geometry still need evaluation.
Bangun Tumpukan Toleransi Terburuk untuk Penyelarasan yang Dapat Diulang
The fit calculation covers only one part of the positioning system. A complete tolerance budget should include every variation capable of moving, tilting, or preventing engagement between the mold halves.
Typical contributors include:
| Kontributor | Kemungkinan Efek |
| Diameter pin | Mengubah izin atau gangguan |
| Lubang atau lubang bushing | Mengubah izin atau gangguan |
| Posisi pemasangan pin | Memindahkan sumbu pencari lokasi |
| Posisi lubang kawin | Memindahkan sumbu penerima |
| Orientasi sumbu | Menciptakan ketidakcocokan sudut atau kontak tepi |
| Bushing diameter luar pas | Mengizinkan atau membatasi gerakan bushing |
| Hubungan bore-to-outside | Mengimbangi lubang bushing fungsional |
| Spasi pola pin | Memengaruhi keterlibatan simultan |
| Suhu pelat cetakan | Mengubah dimensi komponen |
| Memakai | Meningkatkan jarak bebas efektif |
| Puing-puing | Mengurangi jarak bebas yang dapat digunakan atau mencegah tempat duduk penuh |
| Ketidakpastian pengukuran | Mengurangi kepercayaan pada keputusan penerimaan |
A practical worst-case process is:
- Define the maximum permitted alignment variation.
- Identify each dimensional and geometric contributor.
- Calculate the tightest and loosest component fits.
- Add the possible positional and orientation effects.
- Check whether every permissible combination can assemble.
- Reserve allowance for operating temperature, memakai, and contamination.
- Confirm that the inspection system can verify the specified limits.
Worst-case analysis is appropriate when assembly must be guaranteed at every permitted limit. Statistical tolerance analysis may be useful in established, capable production processes, but it should not replace functional verification without a justified process model.
Perbedaan Manufaktur Terpisah dari Variasi Operasi
Manufacturing variation includes:
- component diameter;
- hole diameter;
- posisi fitur;
- ketegak lurus;
- pattern spacing;
- bushing installation position.
Operating variation includes:
- thermal expansion;
- memakai;
- puing-puing;
- kondisi pelumasan;
- plate movement or deformation.
A fit that works during inspection at room temperature may become too tight after heating. A fit that begins with acceptable clearance may lose repeatability as the pin or bushing wears.
Lubrication can reduce friction and seizure risk, but it cannot correct an invalid tolerance stack. Material and hardness affect how well the components retain their dimensions over time, but those decisions should remain separate from the basic fit calculation.
Gunakan tumpukan hipotetis untuk menguji desain
Assume a design permits 0.030 mm of total lateral variation at a functional location.
A simplified hypothetical budget might allocate:
| Kontributor | Efek yang Diizinkan |
| Gerakan radial pin-to-bushing | 0.008 mm |
| Variasi posisi pin | 0.006 mm |
| Variasi posisi bushing | 0.006 mm |
| Orientasi dan efek keterlibatan | 0.004 mm |
| Suhu dan kelonggaran keausan | 0.004 mm |
| Margin desain yang tersisa | 0.002 mm |
If the calculated worst-case total exceeds 0.030 milimeter, the design must change. Possible actions include:
- reducing maximum clearance;
- improving positional control;
- increasing locator spacing;
- using a replaceable bushing;
- revising the relieved-pin geometry;
- reducing operating variation;
- redefining the functional requirement.
The example demonstrates the budgeting method only. Real values must come from the mold’s geometry, kondisi operasi, and manufacturing capability.
Tentukan persyaratan dengan jelas pada gambar atau RFQ
A supplier cannot reliably manufacture or inspect an ambiguous precision requirement.
The drawing or request for quotation should identify:
- nominal pin, hole, and bushing dimensions;
- limit dimensions or an unambiguous fit designation;
- the governing tolerance standard;
- separate mounting-side and locating-side requirements;
- datum fungsional;
- basic feature locations;
- position and orientation tolerances;
- primary and secondary locator roles;
- the orientation of any relieved or flattened pin;
- material and hardness where functionally necessary;
- kondisi perlakuan panas;
- surface finish on locating diameters;
- operating temperature assumptions;
- whether components must be interchangeable;
- whether selective assembly is permitted;
- required inspection characteristics;
- required inspection records;
- whether pins and bushings are supplied as matched components.
The supplier should also know which characteristics are function-critical. A tight pin diameter may be less valuable than a slightly wider size tolerance combined with better positional control.
Hindari Catatan Presisi yang Ambigu
Specifications that need clarification include:
- “high-precision pin” without dimensional limits;
- “±0.005 mm” without naming the controlled feature;
- an ISO fit class without a nominal diameter;
- pin diameter tolerance without a mating-hole tolerance;
- diameter controls without feature-position controls;
- room-temperature dimensions without relevant operating conditions;
- a tolerance with no defined inspection method;
- “100% inspection” without identifying the inspected characteristics.
A numerical tolerance has meaning only when the feature, Tanggal, standar, conditions, and measurement method are clear.
Verify the Pin, Hole, Pattern, and Assembly
Inspection should follow the structure of the specification.
| Persyaratan Terkendali | Arah Verifikasi yang Sesuai |
| Diameter pin | Mengukur di lokasi dan orientasi yang ditentukan |
| Diameter lubang atau bushing | Verifikasi batas lubang dengan metode yang dikalibrasi yang sesuai |
| Posisi pin atau lubang | Ukur relatif terhadap kerangka referensi datum yang dinyatakan |
| Orientasi sumbu | Verifikasi tegak lurus atau hubungan sudut |
| Jarak pola | Mengukur hubungan antara fitur penemuan |
| Keterlibatan lengkap | Gunakan pemeriksaan perakitan terkontrol atau pengukur fungsional jika sesuai |
| Pengulangan | Uji perakitan berulang dalam kondisi yang ditentukan |
No single measurement verifies every requirement.
A micrometer may confirm a pin diameter but cannot establish the pin’s position in the mold plate. A bore measurement may confirm hole size but not perpendicularity. A functional gauge may show that the current assembly engages, but it may not identify which individual feature is approaching its tolerance limit.
The inspection plan should also consider:
- instrument resolution;
- calibration status;
- pemasangan;
- measurement temperature;
- accessibility of the feature;
- measurement uncertainty.
If the measurement uncertainty is too large relative to the tolerance, the conformity decision becomes unreliable. Component conformity also does not automatically prove long-term repeatability under heat, memakai, and repeated mold cycles.
Putuskan apakah komponen standar atau toleransi khusus diperlukan
A standard pin or bushing is suitable when its published dimensions, kelas toleransi, geometri, material, and mounting configuration satisfy the calculated tolerance stack.
Customization may be justified when the design requires:
- a non-standard diameter or locating length;
- separate mounting and locating diameters;
- a special shoulder or flange;
- a defined relieved-pin orientation;
- a specific material or hardness;
- a controlled surface finish;
- unusual retention or removal features;
- a tolerance not available in a standard series.
The decision should start with the functional requirement rather than an assumption that custom parts are automatically more precise. A custom pin still depends on the mating hole, bushing, Sistem Tanggal, dan metode inspeksi.
SunshinePro states that it supplies mold components and supports non-standard accessories based on drawings or samples. Nya Menemukan bushing panduan pin page lists straight, berlapis flange, and custom structures, along with standard or customized sizes. Buyers comparing catalog and drawing-based options can also review the broader guidance on Bagian standar cetakan.
Before ordering, confirm which feature the supplier’s stated tolerance applies to, how it will be inspected, and whether the component must be interchangeable with other pins or bushings.
For a drawing-based review, provide the pin and mating-feature limits, datum scheme, required fit, kondisi operasi, material or hardness requirements, and inspection expectations through the Halaman kontak SunshinePro.
Bagikan:



Ditulis oleh Sunshine
di Sunshine, Kami adalah produsen dan pemasok profesional komponen cetakan presisi, menawarkan berbagai produk untuk aplikasi stamping dan cetakan injeksi. Fokus utama kami adalah mencetak cetakan, pin dan lengan ejector, serta tiang panduan dan bushing. Dengan pemesinan CNC canggih, kontrol kualitas ketat, dan kemampuan produksi yang kuat, kami memastikan keandalan, suku cadang presisi tinggi, bersama dengan komponen standar yang tersedia untuk pasokan global yang cepat dan efisien.
BERITA
DAPATKAN LAYANAN
Dengan suku cadang berkualitas untuk memenuhi setiap anggaran dan staf ramah yang terlatih untuk membuat kunjungan Anda menjadi informatif dan tanpa repot.
