



Desain Kedalaman Tablet Punch Cup: Bentuk, Gaya, dan Risiko Cacat
Tablet punch cup depth helps determine the finished tablet’s face curvature, central band, and overall appearance. A deeper cup can create a more convex tablet, but it may also reduce punch-tip strength and increase sensitivity to capping, uneven density, or wear under certain operating conditions.
There is no universal best cup depth. The correct design depends on cup radius, diameter tablet, land geometry, required compression load, perilaku perumusan, dan kondisi pers. Cup depth should therefore be evaluated as one part of the wider system of Jenis perkakas press tablet, not as an isolated dimension.
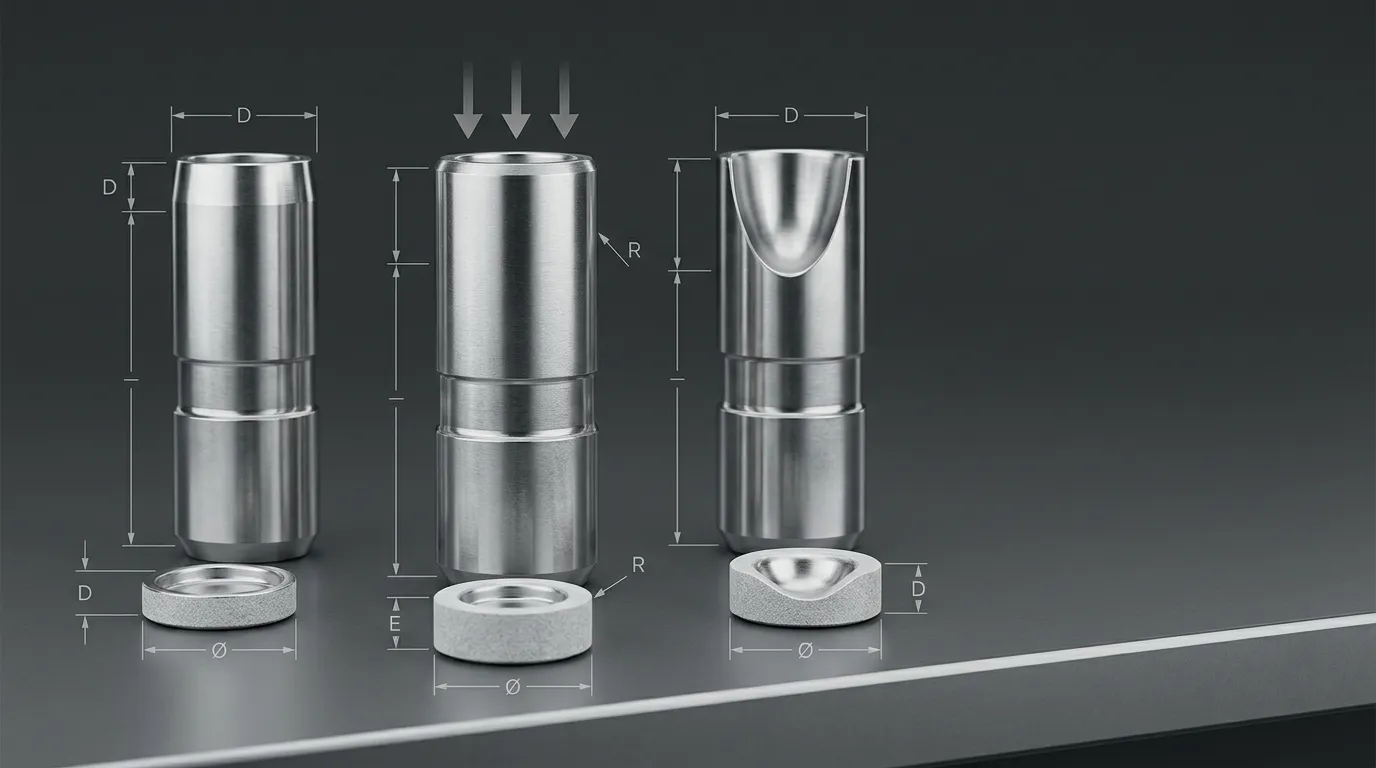
Apa yang diukur kedalaman cangkir punch tablet
The punch cup is the recessed area at the end of the punch tip. During compression, the upper and lower cups form the two main faces of the tablet while the die bore forms its central band or sidewall.
Cup depth is the vertical distance from the highest reference surface of the punch tip to the lowest point of the cup. Identification features such as embossed or debossed letters should not be included in this measurement. This distinction follows the terminology used in the Manual Spesifikasi Tablet APhA.
Cup depth is also separate from punch working length. Working length influences compression position and tablet consistency, while cup depth defines the shape of the tablet face.
Cup Depth, Cup Radius, and Cup Volume Are Different Variables
Cup depth alone does not fully describe the punch profile.
| Variabel | Apa yang dijelaskannya | Mengapa itu penting |
|---|---|---|
| Kedalaman cangkir | Jarak vertikal dari permukaan referensi ke titik terendah cangkir | Influences face height, tablet convexity, and remaining punch-tip section |
| Radius cangkir | Kelengkungan yang digunakan untuk membentuk cangkir | Menentukan seberapa bertahap atau tajam wajah melengkung |
| Volume cangkir | Volume yang terkandung dalam profil tersembunyi | Memengaruhi bagaimana volume tablet didistribusikan antara wajah dan pita tengah |
| Rasio R/D | Radius cangkir dibagi dengan diameter tablet | Membantu membandingkan kelengkungan di seluruh tablet dengan ukuran berbeda |
Two punches can have similar cup depths but different radii. One may use a smooth, broad curve, while another reaches the same depth through a steeper profile. Their tablet appearance, stress distribution, and punch-tip strength may therefore differ.
Compound cups make this distinction even more important. Instead of using one continuous radius, a compound profile combines two or more radii. This can create a smooth-looking tablet face while still producing a steep transition near the outer edge.
Bagaimana cangkir atas dan bawah membentuk pita tablet dan ketebalan total
The finished tablet consists of three connected geometric regions:
- the upper cup-formed face;
- the lower cup-formed face;
- the central band formed inside the die.
For a given total tablet thickness, increasing the combined depth of the upper and lower faces generally leaves less thickness in the central band. A narrower band changes the tablet’s proportions and may influence die-wall contact, perilaku ejeksi, and mechanical failure patterns.
Tablet diameter must also be considered. A 1 mm cup depth does not represent the same curvature on a small tablet and a large tablet. Diameter, radius, kedalaman, and band thickness must be reviewed together.
Upper and lower cup profiles do not always have to match. A tablet may use symmetrical faces, or one side may be flatter to support branding, penanganan, pelapisan, kemasan, or application requirements. Any asymmetrical design should still be evaluated as one complete tablet geometry.
Bagaimana Profil Punch Cup Umum Dibandingkan
The names used for cup profiles describe general forms rather than one universal set of dimensions. A “deep concave” profile from one tooling system or supplier may not have exactly the same depth or radius as another.
| Profil Piala | Bentuk umum | Manfaat desain utama | Batasan atau risiko utama |
| Wajah datar | Permukaan tablet datar | Geometri sederhana dan pemuatan yang relatif langsung | Mungkin tidak memberikan penampilan atau karakteristik penanganan yang diperlukan |
| Flat-faced bevel edge, or FFBE | Pusat datar dengan tepi miring | Mendefinisikan tepi tablet dan dapat mengurangi sudut tajam | Geometri bevel memengaruhi bagian ujung luar dan tepi tablet |
| Flat-faced radius edge, or FFRE | Pusat datar dengan tepi membulat | Memberikan transisi tepi yang lebih halus | Detail jari-jari masih memengaruhi tegangan dan perilaku kompak |
| Cekung dangkal | Wajah tablet yang sedikit cembung | Memberikan kelengkungan sambil mempertahankan pita tengah yang relatif substansial | Mungkin tidak memenuhi persyaratan penampilan yang sangat cembung |
| Cekung standar | Kelengkungan wajah sedang | Menyeimbangkan penampilan dan kepraktisan perkakas umum | "Standar" tidak mewakili satu dimensi universal |
| Cekung dalam | Wajah sangat cembung | Membuat profil tablet yang lebih jelas | Dapat mengurangi kapasitas gaya punch-tip dan meningkatkan sensitivitas terhadap capping |
| Cekung ekstra dalam | Wajah yang sangat cembung | Mendukung bentuk tablet bulat yang khas | Menghasilkan geometri yang lebih agresif dan membutuhkan gaya yang cermat dan tinjauan formulasi |
| Cangkir majemuk | Wajah dibuat dari beberapa jari-jari | Memungkinkan lebih banyak kontrol atas penampilan dan bentuk tepi | Kedalaman saja tidak dapat menggambarkan implikasi stres atau kekuatannya |
A profile should not be selected solely from this classification. The actual drawing must specify the relevant depth, radius or radii, tanah, edge transition, diameter tablet, and total thickness.
Mengapa Geometri Piala yang Lebih Dalam Dapat Mengurangi Kapasitas Gaya Pukulan
The tablet press may be capable of applying a high compression force, but that does not mean every punch-tip design can safely carry that load.
A deeper or steeper cup removes more material from the punch-tip region and changes the path through which compression load passes. The allowable force can depend on:
- tip diameter and shape;
- cup depth and radius;
- single-radius or compound geometry;
- land width and transition geometry;
- punch material and heat treatment;
- existing wear or damage;
- the safety margin applied by the tooling designer.
Specialist tooling guidance consistently warns that machine capacity and punch-tip capacity are separate limits. A tooling design should therefore receive a drawing-specific force assessment rather than relying only on a generic press rating or tooling class.
SunshinePro mencantumkan Premium High-Speed Steel untuk perkakas tekan tablet. Material is one contributor to strength, but it does not replace a geometry-specific review of the punch tip.
Bagaimana transisi darat dan cangkir-ke-tepi memengaruhi kekuatan ujung
The land is the narrow flat area around the perimeter of the punch tip. It provides support at the edge of the cup and influences wear, berkedip, and tablet-band appearance.
A wider or better-supported land may improve edge strength, but changing it can also alter the tablet profile. The transition between the cup and land matters as well. A smooth blend radius generally creates a less abrupt geometric change than a sharp corner.
These details cannot be selected independently:
- Cup depth affects how much material remains beneath the recessed face.
- Land width affects edge support.
- The blend radius affects the transition between the cup and land.
- Tablet appearance limits how much these features can be changed.
There is no universal minimum land width. The correct value depends on the punch shape, material, compression requirement, tablet appearance, dan standar alat.
Compression Force, Pressure, Breaking Force, and Tensile Strength
Several different measurements are used in tablet design, and they should not be treated as synonyms.
| Istilah | Arti |
| Gaya kompresi | The load applied by the tablet press, commonly expressed in kilonewtons |
| Tekanan kompresi | Force divided by an applicable area, commonly expressed in megapascals |
| Gaya putus tablet | Gaya terukur yang diperlukan untuk memecahkan tablet jadi dalam pengujian yang ditentukan |
| Kekuatan tarik | Ukuran yang disesuaikan dengan geometri yang digunakan untuk membandingkan kekuatan mekanik tablet |
Compression pressure is often used in research because the same force produces different pressure conditions on tablets with different face areas.
Breaking force is a direct test result. Tensile strength attempts to account for tablet dimensions and geometry, making it more useful for some comparisons. Highly convex or unusual profiles may require an equation appropriate to that geometry rather than a formula developed for a flat cylindrical tablet.
Bagaimana Kedalaman Cangkir Memengaruhi Mekanika Tablet dan Risiko Cacat
During compression, powder does not densify uniformly in every region of a tablet. Punch shape affects how material moves, how pressure is transmitted, and where density or stress gradients develop.
Finite-element and experimental studies have found that convex punch profiles can produce more heterogeneous density distributions than flat punches. Reduced curvature radius and changes in tablet thickness may increase those gradients under the conditions studied. The effect is important because regions with different density or residual stress may respond differently during decompression and ejection.
These findings are directional, not universal. The actual result also depends on formulation properties, compression pressure, kecepatan, pelumasan, pelepasan udara, diameter tablet, and band thickness.
Mengapa Risiko Pembatasan Tidak Dapat Diprediksi Dari Kedalaman Saja
Capping occurs when part of the upper or lower crown separates from the tablet body. Research published in Penelitian Farmasi found that increasing punch cup depth was associated with a higher capping index in the studied acetaminophen formulation and compression conditions.
Studi terpisah di Jurnal Farmasi Internasional showed that tablet diameter, band thickness, curvature ratio, and their interactions influenced capping behavior. Greater curvature, a thinner band, and larger diameter increased capping susceptibility in that experimental system.
These studies do not prove that every deep cup will cap. They show that geometry can increase risk when combined with particular material and process conditions.
Cup-depth assessment should therefore include:
- diameter tablet;
- upper and lower curvature;
- central band thickness;
- formulation compactibility;
- pemulihan elastis;
- target compression pressure;
- press speed and air-release conditions;
- existing capping history.
A shallower cup may reduce one geometric risk while failing to meet appearance, pelapisan, penanganan, or dosage-form requirements. The design decision is a trade-off, not a simple ranking.
Distinguishing Capping, Laminasi, Air Entrapment, and Tool Wear
Not every separation defect is caused by the cup profile.
| Pengamatan | Kemungkinan penyebab terkait geometri | Kemungkinan penyebab lain | Apa yang harus diverifikasi |
| Mahkota terpisah dari tablet | Aggressive curvature, thin band, konsentrasi tegangan | Pemulihan elastis, entrapped air, unsuitable pressure or speed | Lokasi kegagalan, profil cangkir, respon formulasi, kondisi pers |
| Tablet terpisah melalui bidang internal | Kepadatan atau distribusi tegangan yang tidak merata | Pelumasan, formulation weakness, air pressure | Fracture plane, density pattern, material and process history |
| Bahan tipis muncul di sekitar tali tablet | Damaged or worn land, clearance issue | Die wear, penyelarasan, kekuatan berlebihan | Punch edge, land condition, The Bore, penyelarasan |
| Cacat meningkat setelah penggunaan alat yang lama | Geometri cangkir atau tanah yang efektif telah berubah | Penyimpangan proses atau variasi formulasi | Bandingkan alat yang sudah aus dengan catatan inspeksi asli |
| Kerusakan lokal muncul di dekat tepi tablet | J-hooking atau tepi pukulan yang rusak | Masalah penanganan atau ejeksi | Inspeksi ujung yang diperbesar dan perilaku ejeksi |
Entrapped air is one important non-geometric factor. Research in the Jurnal Ilmu Farmasi shows that internal air pressure can rise during compression and contribute to cracking or capping. Powder permeability, compression speed, tablet size, and consolidation behavior all affect this mechanism.
Cara Memilih Kedalaman Cangkir untuk Tablet Baru atau Revisi
A useful selection process begins with the required tablet, not with a preferred punch profile.
- Define the finished tablet shape and dimensional limits.
- Select depth and radius together.
- Review the remaining band and edge geometry.
- Estimate the required production compression conditions.
- Confirm the allowable force for the proposed punch tip.
- Review formulation and process sensitivity.
- Compare less aggressive alternatives.
- Validate the final design through compression trials and inspection.
Mulailah dengan bentuk dan pita tablet yang diperlukan
Document the dimensions and functional requirements before choosing the cup profile:
- tablet diameter or major and minor axes;
- target total thickness;
- required band thickness;
- upper and lower face shape;
- edge style;
- coating and handling requirements;
- branding or identification area;
- packaging and feeding constraints.
The design team should then determine whether the appearance can be produced with a broader radius or shallower depth. A small geometric change may preserve the visual profile while increasing punch-force margin or reducing capping sensitivity.
Upper and lower profiles should also be assessed separately. A symmetrical tablet may be visually desirable, while an asymmetrical tablet may provide a flatter identification surface or better handling characteristics.
Periksa Formulasi dan Sensitivitas Proses
The same cup geometry can behave differently with two formulations. Relevant material properties include:
- compactibility;
- plastic or brittle deformation behavior;
- pemulihan elastis;
- permeability;
- lubricant sensitivity;
- moisture condition;
- previous capping or lamination history.
Press conditions matter as well. Precompression may assist air release and early consolidation, while press speed affects the time available for densification and decompression. Detailed consolidation-time decisions belong to Kepala pukulan tablet datar dan waktu tinggal, but cup depth should still be reviewed alongside those conditions.
Geometry cannot automatically compensate for a formulation that does not form a stable compact. It also should not be changed before confirming that the defect is not being caused by air entrapment, pelumasan, tekanan, kecepatan, penyelarasan, or worn tooling.
Konfirmasikan margin gaya perkakas dan validasi desain akhir
Before manufacturing the full tooling set, mengonfirmasi:
- the press and tooling standard;
- the proposed upper and lower cup drawings;
- the material and heat-treatment specification;
- the expected operating-force range;
- the allowable punch-tip force for the proposed geometry;
- the required safety margin;
- the cup, tanah, radius, and working-length tolerances;
- the trial and acceptance criteria.
Production trials should use the actual formulation, intended press, realistic operating speed, and expected pressure range. Evaluation should include tablet dimensions, penampilan, breaking behavior, penutupan, laminasi, pengusiran, dan kondisi punch.
A profile is ready for approval only when both sides of the design are acceptable: the punch can withstand the operating conditions, and the formulation can produce a stable tablet with the required shape.
Apa yang Harus Ditentukan pada Gambar Punch dan RFQ
A tooling supplier cannot assess cup depth from a tablet image alone. The RFQ should separate the required tablet geometry from the tooling, pers, dan kondisi produksi.
SunshinePro states that custom tablet tooling can be processed from drawings or samples and that its workflow includes drawing submission, tinjauan desain, kutipan, produksi, inspeksi, and delivery. A controlled drawing remains the clearest way to define the required geometry.
Geometri dan Informasi Aplikasi untuk Disertakan
| Informasi | Mengapa itu penting |
| Diameter tablet atau sumbu mayor dan minor | Menetapkan skala geometri wajah |
| Ketebalan total target | Menentukan profil selesai lengkap |
| Ketebalan pita yang diperlukan | Mengontrol dinding samping tengah dan wilayah kontak mati |
| Kedalaman cangkir atas dan bawah | Mendefinisikan setiap wajah secara independen |
| Jari-jari cangkir atau jari-jari majemuk | Menggambarkan kelengkungan daripada kedalaman saja |
| Lebar tanah | Mendefinisikan dukungan punch-edge dan tepi tablet |
| Radius campuran atau transisi | Mengontrol transisi cangkir ke darat |
| Gaya tepi | Memengaruhi tepi tablet dan geometri pukulan |
| Embossing atau debossing | Mengubah geometri lokal dan fitur identifikasi |
| Standar mesin cetak dan perkakas tablet | Mengonfirmasi kompatibilitas fisik |
| Gaya atau rentang tekanan yang diharapkan | Mendukung tinjauan kekuatan perkakas |
| Formulasi dan riwayat cacat yang diketahui | Mengidentifikasi risiko khusus aplikasi |
| Persyaratan permukaan dan inspeksi | Menetapkan kriteria penerimaan |
A supplier should also know whether an existing tablet or punch sample is being reproduced. A sample may help communicate shape, but it should not replace a controlled drawing when exact depth, radius, tanah, and tolerance matter.
Toleransi, Inspeksi, and Documentation Requirements
Feature-specific tolerances should be agreed on the drawing. A general supplier capability does not prove that every cup feature can or should use the same tolerance.
Define how the following will be checked:
- upper and lower cup depth;
- cup radius or profile;
- land width;
- tip dimensions;
- panjang kerja;
- panjang keseluruhan;
- consistency across the punch set;
- material identification;
- final inspection records.
SunshinePro’s tablet tooling page publishes a general tolerance capability of ±0.002 mm and states that material inspection reports can be provided. That figure should still be confirmed against the actual cup feature, drawing geometry, metode inspeksi, and production requirement.
Itu menyatakan pendekatan kontrol kualitas includes raw-material inspection, pemantauan dalam proses, pengujian akhir, dan pelaporan inspeksi. Buyers should specify which records are required for the particular tooling order.
Bagaimana Keausan Dapat Mengubah Kedalaman Cangkir Efektif dan Risiko Cacat
An approved cup design can change during production life.
Repeated polishing may gradually reduce effective cup depth, alter the radius, narrow the land, or round the edge transition. Uneven wear across a punch set can also produce differences in tablet thickness or face shape.
Common wear-related warning signs include:
| Gejala produksi | Pemeriksaan perkakas |
| Wajah tablet menjadi kurang jelas | Bandingkan kedalaman dan profil cangkir dengan gambar yang disetujui |
| Perubahan tampilan pita tablet | Inspect land width, edge transition, dan kondisi cetakan |
| Capping muncul setelah periode produksi yang stabil | Check for J-hooking, worn land, altered cup geometry, and process drift |
| Dimensi bervariasi menurut stasiun | Bandingkan pukulan di seluruh set lengkap |
| Berkedip muncul di sekitar pita | Inspect punch-tip edges, Pembersihan, memakai, dan penyelarasan |
J-hooking occurs when the punch-tip edge becomes deformed or develops a hooked profile. This damaged edge may disturb tablet release and contribute to capping, laminasi, or flashing.
Before redesigning the cup, compare the current tooling with its original measurement and inspection records. A design that performed correctly when new may be experiencing a maintenance or wear problem rather than a fundamental geometry error.
Kesalahan Umum Desain Kedalaman Cangkir
- Memilih kedalaman dari tampilan tablet saja
Appearance does not reveal punch-tip strength, density distribution, or formulation sensitivity. - Memperlakukan kedalaman dan jari-jari sebagai dapat dipertukarkan
Two profiles with the same depth can have different curvature and stress behavior. - Mengabaikan diameter tablet
A fixed depth has a different meaning on different tablet sizes. - Mengabaikan pita tengah
Deeper faces may reduce band thickness and change mechanical behavior. - Menggunakan kapasitas alat berat sebagai batas punch-force
The press may be able to apply more load than the punch tip can safely withstand. - Membiarkan detail tanah dan transisi tidak didefinisikan
The cup edge is part of the structural design, not a minor finishing feature. - Dengan asumsi semua cangkir dalam menyebabkan capping
Depth may increase susceptibility, but formulation and process conditions determine the actual result. - Dengan asumsi cangkir dangkal menghilangkan cacat
Capping and lamination can still result from air, pemulihan elastis, pelumasan, tekanan, memakai, or other causes. - Menyalin profil dari diameter tablet lain
The depth-to-diameter and radius-to-diameter relationships may be different. - Mengabaikan keausan alat
A worn punch may no longer match the approved cup profile. - Menerapkan toleransi umum untuk setiap fitur
Kedalaman cangkir, radius, tanah, and working length may require different controls. - Menyetujui gambar tanpa uji coba yang relevan dengan produksi
Dimensional correctness does not prove formulation compatibility.
Kapan Harus Melibatkan Pemasok Perkakas Tablet
Supplier review is useful when the cup is deep, compound, asymmetrical, unusually small, intended for high compression load, or associated with recurring tablet defects. It is also appropriate when an existing punch or tablet sample must be reproduced.
SunshinePro perkakas tekan tablet page confirms punches and dies, Baja Berkecepatan Tinggi Premium, standard and non-standard size options, and customization based on drawings or samples. It also states that material inspection reports are available.
Before placing an order, request drawing-specific confirmation of:
- upper and lower cup geometry;
- material;
- feature tolerances;
- press and tooling compatibility;
- metode inspeksi;
- documentation;
- allowable punch-tip force.
SunshinePro does not publicly confirm formulation testing, finite-element analysis, capping trials, or pharmaceutical-process validation. Those requirements should be discussed and verified separately rather than assumed from its general tooling capabilities.
Once the tablet geometry, expected operating conditions, and inspection requirements are defined, Kirim gambar atau sampel perkakas for manufacturing review and quotation.
Bagikan:



Ditulis oleh Sunshine
di Sunshine, Kami adalah produsen dan pemasok profesional komponen cetakan presisi, menawarkan berbagai produk untuk aplikasi stamping dan cetakan injeksi. Fokus utama kami adalah mencetak cetakan, pin dan lengan ejector, serta tiang panduan dan bushing. Dengan pemesinan CNC canggih, kontrol kualitas ketat, dan kemampuan produksi yang kuat, kami memastikan keandalan, suku cadang presisi tinggi, bersama dengan komponen standar yang tersedia untuk pasokan global yang cepat dan efisien.
BERITA
DAPATKAN LAYANAN
Dengan suku cadang berkualitas untuk memenuhi setiap anggaran dan staf ramah yang terlatih untuk membuat kunjungan Anda menjadi informatif dan tanpa repot.
