



Pelapis Punch Tablet untuk Masalah Menempel dan Memetik
Tablet punch coatings can reduce some sticking and picking problems, but they are not a universal cure. Material may adhere to a punch because of formulation moisture, pelumasan yang tidak memadai, panas, kondisi pers, damaged tooling, unsuitable embossing, or the interaction between the formulation and punch surface. A coating should be selected only after these causes have been investigated.
Surface treatment is also only one part of the broader tooling decision. Different Jenis perkakas press tablet involve different punch geometries, dimensi, substrates, dan kebutuhan operasional. This guide focuses specifically on deciding whether a punch coating is appropriate, comparing common coating families, specifying the coated tool, and evaluating the result under production conditions.
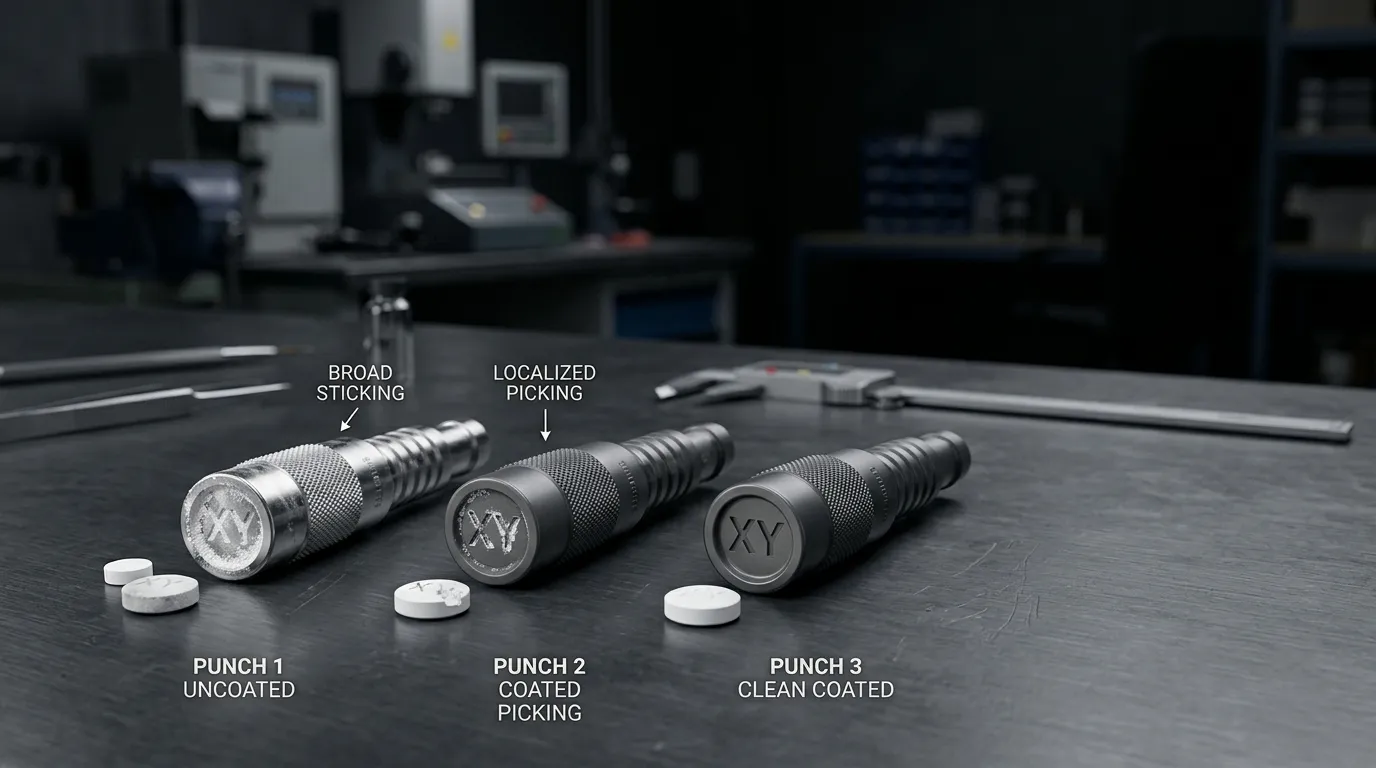
Identifikasi Masalah Sebelum Memilih Punch Coating
Sticking occurs when formulation material adheres to the punch face instead of remaining fully within the compressed tablet. The deposit may begin as a thin film and gradually become a visible layer that affects tablet appearance, weight consistency, kualitas permukaan, or press operation.
Picking is more localized. Material is pulled from the tablet surface and collects inside or around recessed punch features such as letters, logos, garis skor, and small decorative details. A tablet may therefore show a damaged character or crater even when the rest of its surface appears acceptable.
The distinction matters because a coating selected for broad punch-face adhesion may not correct picking caused by sharp embossing corners, damaged lettering, or material trapped inside a narrow recess.
Menempel, Memetik, and Filming Are Not the Same Defect
| Gejala | Lokasi khas | Pemeriksaan pertama | Kemungkinan relevansi lapisan |
|---|---|---|---|
| Pembuatan film | Lapisan tipis di sebagian atau seluruh permukaan pukulan | Check early buildup, kelembapan, pelumasan, punch cleanliness, dan kondisi permukaan | Tanda peringatan yang dapat membenarkan uji coba permukaan setelah penyebab dasar dikendalikan |
| Menempel | Area cangkir atau wajah punch yang lebih luas | Review formulation properties, panas, tekanan, kekasaran, korosi, and run conditions | Pelapisan dapat membantu ketika adhesi permukaan yang persisten tetap ada setelah koreksi proses |
| Memetik | Timbul, logos, garis skor, or recessed details | Inspect character geometry, damaged edges, menggosok, and local material accumulation | Selective coating or a different surface system may help, but design changes may also be necessary |
The underlying mechanism involves competition between adhesion to the punch and cohesion within the compact. When formulation-to-tool adhesion becomes strong enough, material stays on the punch or is pulled from the tablet. Itu Ulasan IQ Consortium tentang menempelkan dan memetik tablet describes the defect as a multifactorial problem involving API properties, formulasi, perkakas, the tablet press, and processing conditions.
Putuskan apakah pelapisan adalah tindakan berikutnya yang benar
A coating request should begin with a root-cause review. Selain itu, an expensive surface treatment may be used to compensate for a correctable formulation, equipment, or maintenance problem.
Check the following before comparing coating quotations:
- Inspect the punch surface. Look for scratches, corrosion pits, damaged polish, embedded residue, worn lettering, tepi terkelupas, and local roughness. Surface defects can hold particles and create repeated buildup sites.
- Review moisture and hygroscopicity. A wet granulation, moisture-sensitive API, humid room, or condensation on cold tooling can increase adhesion. A coating cannot provide reliable control if the material condition changes significantly between batches.
- Tinjau pelumasan. Jenis pelumas, jumlah, distribution, and blending can affect punch adhesion. Correcting lubrication requires formulation expertise because excessive or prolonged lubrication can create other tablet-quality problems.
- Check temperature and press conditions. Low-melting ingredients, extended compression, high operating speed, gesekan, and heat accumulation can change the formulation’s behavior at the punch face.
- Examine cup and embossing geometry. Deep cups, narrow recesses, sharp character corners, and small lettering may concentrate material or make cleaning difficult.
- Compare when the defect begins. Immediate buildup may suggest a different mechanism from adhesion that develops only after a long production run.
- Confirm tooling cleanliness and handling. Kontaminasi, improper storage, or unsuitable polishing can produce a surface that behaves differently from a new tool.
Kondisi yang harus diperbaiki sebelum pelapisan
Coating should not be the first response when the main problem is:
- uncontrolled blend moisture or room humidity;
- pelumasan tidak konsisten;
- residue from inadequate cleaning;
- visibly scratched, corroded, atau alat yang rusak;
- worn or unsuitable embossing;
- unstable press temperature or compression conditions;
- a formulation change that has not been evaluated;
- buildup caused by a specific mechanical defect.
These factors may remain active after coating and can shorten coating life or make a trial result difficult to interpret. Practical root-cause resources such as the Empat belas penyebab tablet menempel dan memetik show why tooling surface treatment should be considered within a wider process investigation.
Kondisi yang membenarkan evaluasi lapisan
A controlled coating trial becomes more reasonable when:
- sticking persists after moisture, pelumasan, pembersihan, and press conditions have been stabilized;
- picking repeatedly occurs around fine embossed details;
- an abrasive formulation gradually damages the punch finish;
- corrosion creates pits that encourage further buildup;
- the current surface loses its finish too quickly during production;
- a documented formulation-to-surface interaction remains after other causes are addressed.
Even in these cases, coating should be treated as one part of the corrective plan rather than a guaranteed solution.
Tentukan Fungsi Pelapisan yang Diperlukan
Buyers often begin by asking for a named coating. A better first question is: What must the surface do?
| Fungsi yang diperlukan | Masalah utama ditangani | Masalah pemilihan penting |
| Performa anti lengket | Adhesi dan penumpukan formulasi | Surface chemistry, menyelesaikan, tekstur, sifat formulasi, coated area |
| Ketahanan aus | Kerusakan abrasif dan hilangnya detail pukulan | Kekerasan, adhesi pelapis, substrate support, ketebalan lapisan |
| Ketahanan korosi | Chemical attack, pewarnaan, and pitting | Coating continuity, exposed edges, cleaning environment, formulation chemistry |
| Perlindungan gabungan | Adhesi ditambah keausan atau korosi | Trade-offs among finish, daya tahan, dimensional control, dan pemeliharaan |
A very hard coating is not automatically the best anti-stick coating. Hardness mainly describes resistance to indentation or wear under a defined test method. Sticking also depends on surface chemistry, menyelesaikan, topography, sifat formulasi, tekanan, suhu, dan pelumasan.
A surface can be hard but still attract or mechanically trap a particular formulation. sebaliknya, a coating marketed for low adhesion may fail prematurely if it lacks sufficient wear resistance for an abrasive product.
Surface energy is another useful concept, but it should not be used as a single selection number. Research comparing differently coated punches found that formulation and coating interactions could not be predicted reliably from one surface property alone. The comparative Studi Punch-coating ibuprofen supports formulation-specific evaluation rather than a universal ranking.
Bandingkan Opsi Pelapisan Punch Tablet Umum
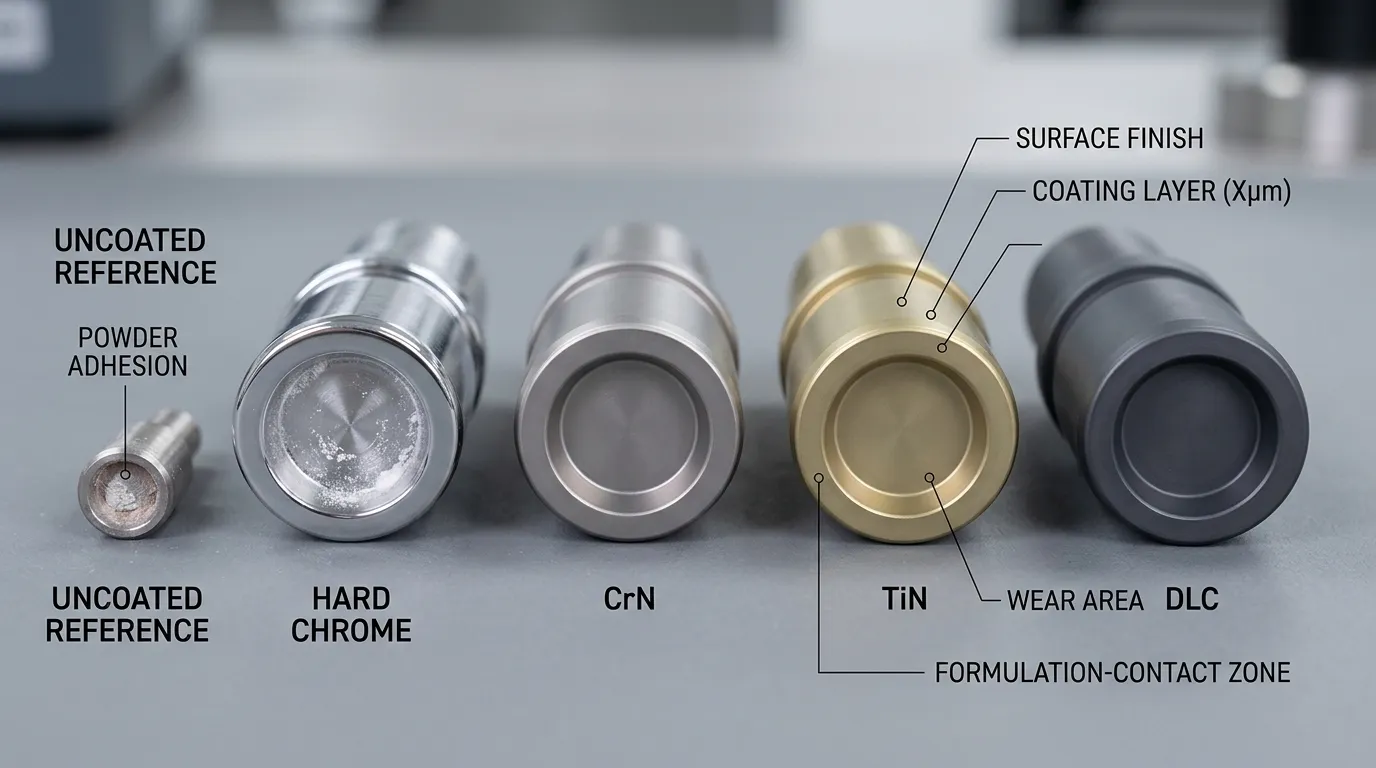
Krom keras, chromium nitride, titanium nitride, diamond-like carbon, and proprietary textured systems frequently appear in tablet tooling discussions. Their names alone do not provide enough information for selection.
| Keluarga pelapis | Posisi umum | Potensi keuntungan | Pertanyaan dan batasan |
| Krom keras | Traditional plated surface for wear, menyelesaikan, and corrosion protection | Established process; can provide a hard, polishable surface | Thickness distribution, cacat permukaan, edge buildup, post-polishing, and coating continuity must be controlled |
| Kromium nitrida | PVD coating often evaluated for adhesion, memakai, and corrosion requirements | Dapat menggabungkan beberapa fungsi permukaan tergantung pada sistem | CrN standar dan CrN multilayer atau bertekstur eksklusif belum tentu setara |
| Titanium nitrida | Lapisan PVD keras umumnya dikaitkan dengan ketahanan aus abrasif | Berguna di mana pelestarian geometri dan ketahanan aus mendominasi | Kekerasan tinggi saja tidak membuktikan kesesuaian anti-lengket |
| Karbon seperti berlian | Keluarga sistem pelapisan berbasis karbon | Dapat memberikan sifat keausan dan interaksi permukaan yang berguna | DLC composition, struktur lapisan, deposition method, and substrate compatibility vary by supplier |
| Sistem bertekstur atau multilayer eksklusif | Kombinasi kimia pelapis dan permukaan yang direkayasa yang dikembangkan pemasok | Dapat menargetkan mekanisme atau formulasi lengket tertentu | Harus dinilai menggunakan dokumentasi khusus produk dan uji coba yang representatif |
Chrome Keras
Hard chromium is normally deposited by electroplating. It has a long history as a hard, corrosion-resistant surface treatment, but its performance depends on preparation, plating quality, thickness distribution, and final finishing.
For tablet punches, buyers should ask whether plating changes sharp edges, land areas, character details, or final dimensions. Surface pits, microdefects, and inconsistent coverage can become weak points or particle-retention sites. Polishing may improve the final finish, but it can also alter coating thickness or detailed features when poorly controlled.
Hard chrome should therefore be judged as a complete plated and finished system, not only by the word “chrome.”
Kromium Nitrida
Chromium nitride is commonly applied through physical vapor deposition, or PVD. It is frequently considered where sticking, keausan abrasif, and corrosion resistance overlap.
CrN should not be treated as one standardized product. Different suppliers may use different pretreatments, layer structures, ketebalan-ketebalan, deposition conditions, and final finishes. Some proprietary systems also combine CrN chemistry with engineered surface texture.
This means performance data from one branded CrN system cannot automatically be transferred to another. The coating must be assessed with the actual formulation, desain punch, substrat, dan kondisi produksi.
Titanium Nitrida
Titanium nitride is widely recognized as a hard, wear-resistant PVD coating. It may be relevant when an abrasive formulation wears the punch face, lettering, or cup geometry.
Its hardness can make it attractive in comparison tables, but sticking is not purely a wear problem. A TiN-coated punch may still show adhesion if its surface chemistry, menyelesaikan, or formulation interaction is unsuitable.
TiN should be shortlisted when wear resistance is a primary objective, then tested for adhesion under the intended application rather than assumed to be an anti-stick solution.
Karbon seperti berlian dan sistem permukaan eksklusif
DLC refers to a family of carbon-based coatings rather than one uniform material. Suppliers may offer different compositions, layer structures, deposition methods, ketebalan-ketebalan, and surface finishes under the same broad category.
The same caution applies to proprietary multilayer or textured surfaces. A supplier may combine coating chemistry with a controlled topography designed for a particular sticking mechanism. That system should be evaluated according to its own documentation and trial data, not treated as identical to generic CrN, TiN, atau DLC.
Artikel spesialis Memilih Pelapis untuk Meningkatkan Kinerja Perkakas Tablet highlights the importance of coating adhesion, kondisi substrat, finishing permukaan, suhu proses, stabilitas dimensi, and uniformity. These engineering factors are often more useful than a simple list of coating trade names.
Match the Coating to the Formulation, Perkakas, and Application
Coating selection should reflect the actual failure environment.
A hygroscopic formulation may require better moisture control before any surface trial. A low-melting API may become more adhesive as compression and tooling temperatures rise. An abrasive mineral or nutraceutical formulation may require greater wear resistance to keep the punch surface smooth. A corrosive formulation may need a continuous protective barrier that prevents pits from developing.
Punch design changes the local conditions as well. Deep cups, detailed logos, narrow score lines, and small characters create different contact and release patterns from a simple flat-faced tool. Picking inside one letter may call for a different response from general filming across an entire punch cup.
Production conditions also matter. A coating that performs acceptably during a short, low-speed trial may behave differently during an extended run at commercial speed. The test should reproduce the pressure, panas, cleaning cycle, and duration that contribute to the real problem.
Mengapa Pemilihan Substrat Datang Sebelum Perawatan Permukaan
The coating depends on the base tool for support. Baja perkakas, perlakuan panas, kekerasan, kondisi tempering, kebersihan, persiapan permukaan, and existing damage can all affect coating adhesion and durability.
A coating cannot restore a punch that is dimensionally unsuitable, heavily worn, retak, or improperly heat-treated. The coating process itself may also expose the tool to preparation or deposition conditions that must be compatible with the substrate.
Pemilihan nilai terperinci termasuk dalam Pemilihan baja perkakas tablet decision. For coating purposes, the essential questions are:
- What is the exact substrate?
- How was it heat-treated?
- What is its current surface and dimensional condition?
- Is the coating process compatible with that substrate?
- Will the final coating and finishing steps preserve the required geometry?
Specify the Coating, Coated Area, and Final Tool Requirements
A useful quotation request should define more than “anti-stick coating.” The buyer and supplier should agree on the functional and dimensional requirements of the finished punch.
Specify or request clarification on:
- the required function: anti-stick, memakai, korosi, or combined protection;
- the coating family or proposed proprietary system;
- the deposition process;
- the exact coated area;
- whether coverage includes only the punch tip and cup or other tool regions;
- masking requirements;
- nominal coating thickness and allowable variation;
- surface finish before and after coating;
- treatment of embossing, garis skor, sudut-sudut tajam, and edges;
- final punch dimensions after coating;
- coating adhesion or integrity inspection;
- substrate identification and heat-treatment condition;
- pembersihan, pemolesan, penanganan, and storage restrictions;
- wear-through and recoating criteria.
Selective coating can be useful when the problem is limited to the formulation-contact area. All-over coating may create different dimensional, penanganan, or cost considerations. The correct approach depends on the tool design and coating process.
Fine embossing deserves particular attention. Excessive buildup at an edge or inside a recess may reduce character clarity even when the rest of the coating is acceptable. The final inspection should therefore cover both overall dimensions and local detail.
SunshinePro menyatakan bahwa perkakas tekan tablet can be custom processed from drawings or samples and that material inspection reports can be provided. Its product page also lists high-speed steel, Pemesinan CNC, perlakuan panas, custom sizes, and tablet punching-head customization. These verified tooling capabilities do not, sendiri, confirm the availability of any named coating or coating-deposition process.
Evaluasi Pemasok Pelapis dan Kutipan
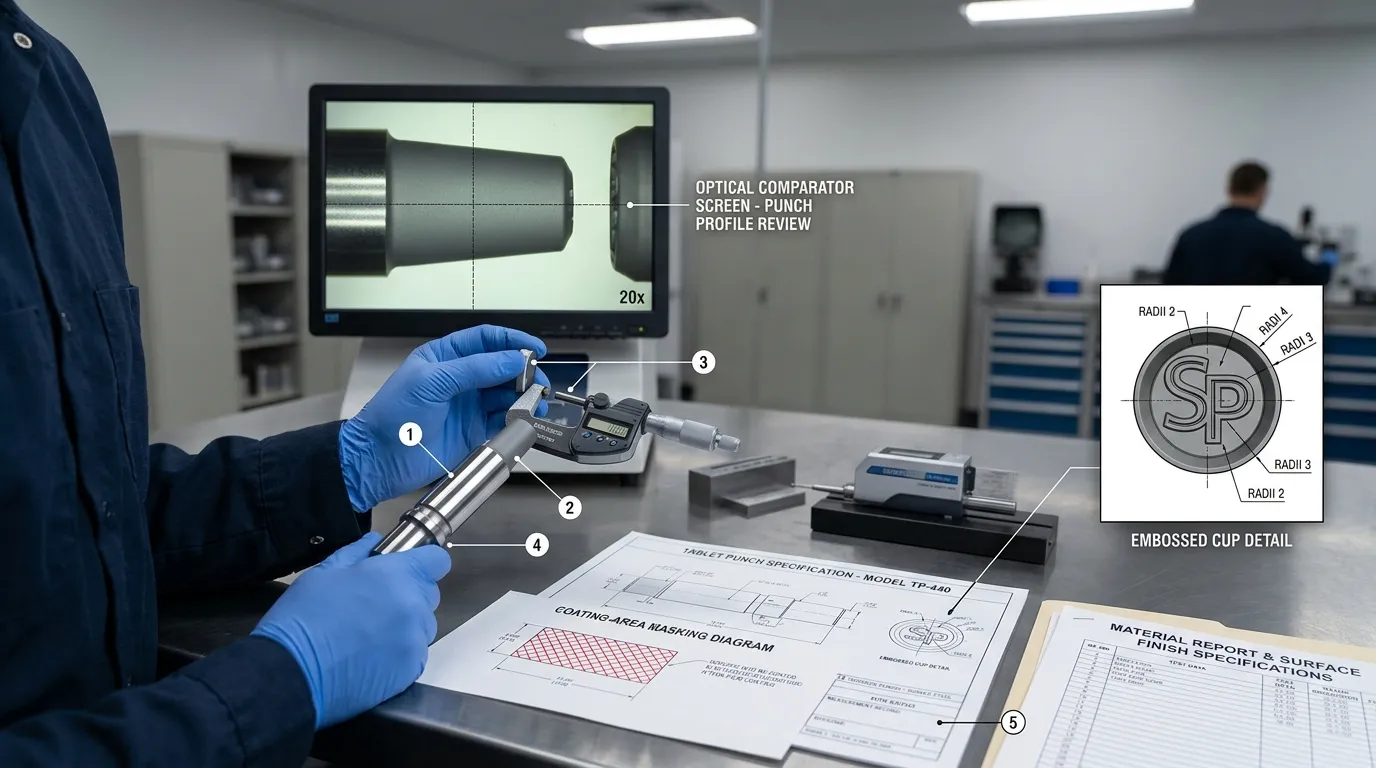
A strong supplier proposal should connect the recommended surface to the buyer’s formulation, perkakas, failure pattern, dan kondisi produksi. A coating name and hardness claim are not enough.
Informasi untuk Disertakan dalam RFQ
Berikan kepada pemasok:
- formulation type and known adhesion behavior;
- whether the problem is sticking, memetik, or filming;
- the exact location of buildup;
- how quickly the deposit develops;
- current punch material and heat-treatment information;
- photographs of the buildup and worn tooling;
- punch drawings, cup geometry, embossing, and score details;
- tablet press model or applicable tooling standard;
- operating speed and relevant compression conditions;
- cleaning and polishing methods;
- current coating or uncoated baseline;
- known moisture, suhu, memakai, or corrosion concerns;
- the main objective: reduced adhesion, improved wear, corrosion protection, or a combination.
This information allows the supplier to evaluate the complete application instead of recommending a standard coating based only on the tablet shape.
Dokumen dan jawaban atas permintaan dari pemasok
Minta pemasok untuk mengidentifikasi:
- the exact coating or proprietary system;
- the deposition process;
- compatible substrates and heat-treatment conditions;
- the areas that will be coated or masked;
- coating thickness and variation;
- expected final surface condition;
- how coating adhesion and integrity are inspected;
- how final punch dimensions and detailed features are checked;
- any prohibited cleaning or polishing method;
- how wear-through is identified;
- whether recoating is possible;
- what preparation is required for used tools;
- which material, proses, and inspection records are available.
Any performance figure should be accompanied by test conditions. A service-life claim based on one abrasive formulation, pers, and cleaning routine may not apply to another application.
Regulatory suitability should also be reviewed using coating-specific documentation. General quality certifications or broad material statements do not prove that a surface is acceptable for every pharmaceutical product, API, market, or cleaning process.
Validasi lapisan dalam kondisi produksi yang representatif
A coating should be compared under controlled conditions before it is adopted across a full tooling set.
- Establish a baseline. Record the performance of the current uncoated or existing coated tools.
- Define the acceptance criteria. Decide in advance what will be measured, such as buildup location, time before cleaning, tablet-surface quality, embossing clarity, keausan alat, or coating damage.
- Control important variables. Keep the formulation, pers, geometri perkakas, kondisi operasi, and cleaning procedure as consistent as practical.
- Test under representative conditions. Use production-relevant speed, kompresi, panas, and run duration rather than relying only on a short laboratory test.
- Record the defect progression. Note when buildup begins, where it appears, and whether it stabilizes or worsens.
- Inspect the coating after the run. Look for scratches, wear-through, mengelupas, peeling, retakan, perubahan warna, and local loss around embossing.
- Compare the complete result. An apparent reduction in sticking should not be accepted if it introduces dimensional problems, damaged details, difficult cleaning, or coating-integrity concerns.
Pekerjaan yang ditinjau sejawat menggunakan Kotak alat kompresi untuk membandingkan pelapis perkakas supports controlled comparison rather than assumptions based on coating labels. A trial with one formulation should also not be treated as proof that the coating will perform equally well with another API or process.
Pertahankan pukulan berlapis tanpa merusak permukaan fungsional
Coated punches may require different maintenance from uncoated tools. Cleaning or polishing methods that are safe for bare steel may scratch, tipis, or remove a functional coating.
Follow the coating supplier’s instructions and avoid assuming that one procedure applies to every surface. Maintenance should include inspection for:
- localized wear-through;
- scratches or abrasion;
- keripik, retakan, or peeling;
- corrosion near uncoated edges;
- loss of embossing clarity;
- increased cleaning frequency;
- renewed sticking in previously stable areas;
- damage caused by handling or storage.
The location of renewed buildup can help diagnose coating wear. If adhesion returns first around a letter edge or score line, the local surface may have worn or been damaged even when the wider punch face still looks acceptable.
Recoating is not always the correct response. The supplier should inspect the substrate, remaining dimensions, kerusakan permukaan, and detailed geometry before deciding whether stripping and recoating are technically suitable. Worn or damaged tools may need replacement instead.
Gunakan pemilihan pelapis sebagai bagian dari keputusan perkakas lengkap
A defensible coating decision follows a clear sequence:
- identify whether the defect is sticking, memetik, or filming;
- correct formulation, pembersihan, proses, and damaged-tooling causes;
- define whether anti-stick, memakai, korosi, or combined protection is required;
- match the coating system to the formulation, substrat, geometri, dan kondisi produksi;
- specify the coated area, finishing permukaan, dimensi, dan dokumentasi yang diperlukan;
- compare supplier proposals using the same criteria;
- validate the selected surface against an established baseline;
- maintain and inspect the coated tools according to supplier instructions.
SunshinePro’s website confirms custom tablet punches and dies made from drawings or samples, with high-speed steel, Pemesinan CNC, perlakuan panas, kustomisasi, and material inspection reports listed on its tablet tooling page. It does not currently verify a named tablet punch coating portfolio, so coating availability and technical details should be confirmed for the specific inquiry.
To discuss the base tooling, gambar-gambar, dimensi, persyaratan material, and operating context, kirimkan persyaratan perkakas Anda ke SunshinePro. Include the sticking or picking pattern and the coating questions from this guide so the technical review can begin with the actual application rather than a generic coating request.
Bagikan:



Ditulis oleh Sunshine
di Sunshine, Kami adalah produsen dan pemasok profesional komponen cetakan presisi, menawarkan berbagai produk untuk aplikasi stamping dan cetakan injeksi. Fokus utama kami adalah mencetak cetakan, pin dan lengan ejector, serta tiang panduan dan bushing. Dengan pemesinan CNC canggih, kontrol kualitas ketat, dan kemampuan produksi yang kuat, kami memastikan keandalan, suku cadang presisi tinggi, bersama dengan komponen standar yang tersedia untuk pasokan global yang cepat dan efisien.
BERITA
DAPATKAN LAYANAN
Dengan suku cadang berkualitas untuk memenuhi setiap anggaran dan staf ramah yang terlatih untuk membuat kunjungan Anda menjadi informatif dan tanpa repot.
