



Daftar Periksa Inspeksi Punch Pin untuk QC Masuk dan Rutin
A punch pin inspection checklist should answer four questions: Is this the correct punch? Does it match the approved specification? Is it still fit for service? What action should follow the inspection?
This guide covers individual punch pins used in metal-stamping dies. Incoming QC verifies a newly supplied punch against the purchase order, gambar, revision, and required documentation. Routine QC checks whether a punch remains serviceable after production use, menggiling ulang, a collision, or another abnormal event.
Punch pins work within a larger die system. Guides, bushing, retainers, stripper components, Pembersihan, and alignment can all influence punch condition. The broader roles of these components are covered in the Panduan Komponen Die (disimpulkan). Ini, the focus stays on inspecting and dispositioning the punch pin itself.
No universal tolerance, inspection interval, or wear limit applies to every punch pin. Acceptance must be based on the approved drawing, purchase specification, control plan, or another documented requirement.
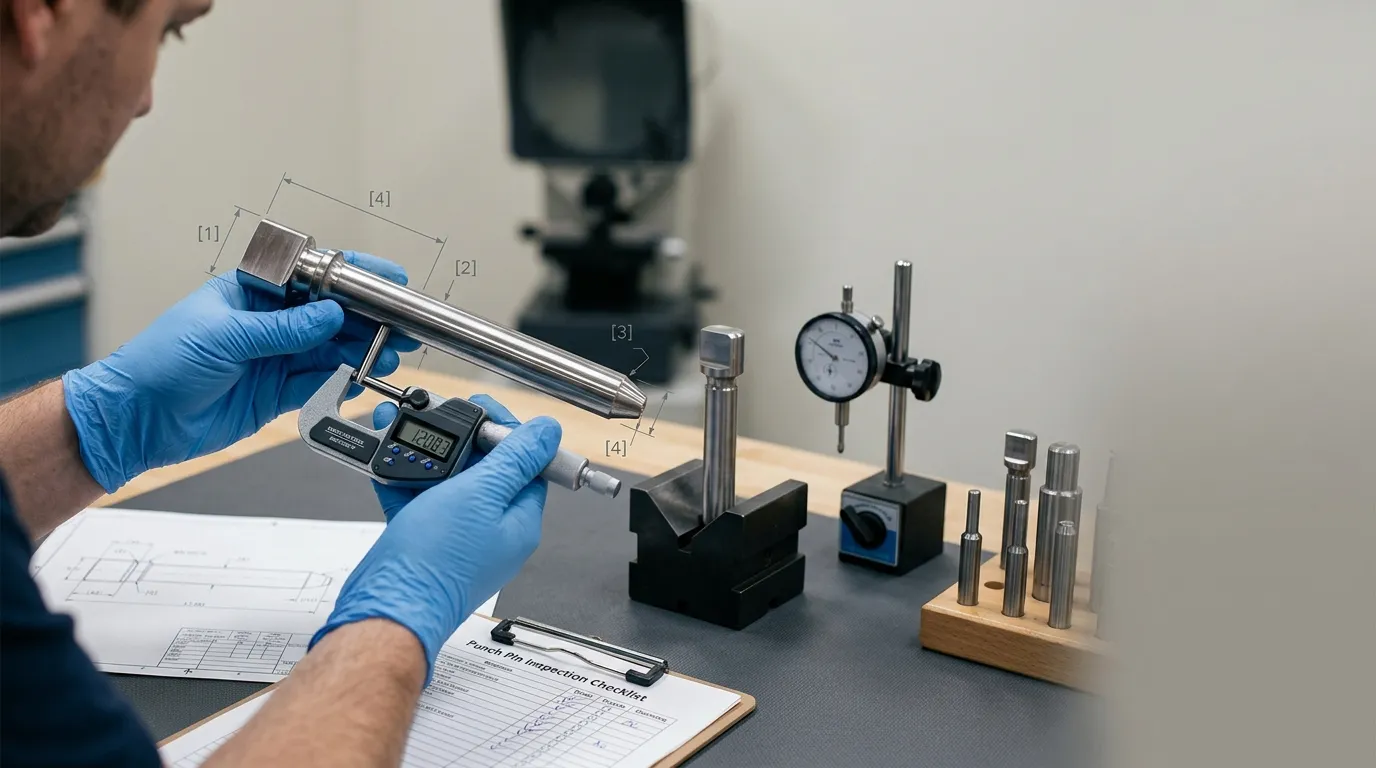
QC Masuk dan QC Rutin Memeriksa Risiko yang Berbeda
Incoming and routine inspection use many of the same instruments, but they answer different questions.
| Tahap inspeksi | Tujuan utama | Pemeriksaan umum | Keputusan utama |
|---|---|---|---|
| QC Masuk | Konfirmasikan bahwa pukulan yang disediakan sesuai dengan pesanan dan spesifikasi yang disetujui | Part identity, revisi gambar, material or coating documents, visible damage, dimensi, geometri, inspection report | Accept, hold, return, or reject |
| QC Rutin | Konfirmasikan bahwa pukulan bekas tetap aman dan berfungsi | Keausan tepi, retakan, menyebalkan, perubahan dimensi, kehabisan, panjang kerja, gejala produksi, regrind history | Kembali ke layanan, monitor, regrind, mengganti, or investigate |
| Inspeksi pasca-penggilingan ulang | Konfirmasikan bahwa penajaman mengembalikan tepi tanpa membuat fitur lain tidak dapat diterima | Edge form, burr removal, panjang keseluruhan, panjang kerja, profil, kondisi permukaan | Release, pengolahan ulang, or replace |
| Inspeksi pasca-acara | Check for hidden or visible damage after a jam, tabrakan, misfeed, or nearby breakage | retakan, membengkokkan, head damage, kehabisan, permukaan tempat duduk, komponen pengikatan | Karantina, menyelidiki, memperbaiki, or replace |
Incoming inspection should establish a reliable baseline. Recording the punch’s as-received dimensions and condition makes later wear easier to identify.
Routine inspection compares the current punch against that baseline and any approved service limits. A punch can remain within its original manufacturing tolerance yet show an abnormal wear trend. sebaliknya, a worn feature may still appear visually acceptable while no longer meeting the documented service requirement.
Prepare the Punch, Dokumen, and Measuring Equipment
Inspection should not begin with a caliper. It should begin with the correct documents, part identity, and measurement conditions.
- Confirm the inspection stage. Record whether the punch is incoming, in routine service, newly reground, or being checked after an abnormal event.
- Obtain the approved drawing. Verify the drawing number and revision before measuring anything. An accurate measurement against an obsolete revision is still an invalid inspection result.
- Review the purchase and quality requirements. Check the purchase order, control plan, approved sample, inspection-report requirement, and any requested material, perlakuan panas, kekerasan, or coating documentation.
- Match the punch to its records. Confirm the part number, lot or serial number, kuantitas, material designation, coating designation, and any engraved identification.
- Inspect the packaging before cleaning. Record impact damage, korosi, broken protective packaging, loose punches, or signs that sharp edges contacted each other during transport.
- Clean the punch carefully. Hilangkan minyak, kotoran, keripik, and transferred material without rounding the cutting edge or scratching a coated surface. Residue on a diameter or seating face can affect the measurement.
- Stabilize the part when tolerances are tight. A punch arriving from a hot production area, cold warehouse, or vehicle may need time to reach the inspection environment. Temperature differences can affect dimensional results.
- Verify the measuring equipment. Check instrument identification, status kalibrasi, measuring range, penyelesaian, kondisi kontak, and cleanliness. Confirm that any V-block, pusat, perlengkapan, or surface plate is also clean and suitable for the feature.
SunshinePro states that non-standard mold parts can be processed from customer drawings, while its punch-pin page lists diameter, panjang, gaya kepala, kelas material, and coating as customizable characteristics. Those fields should therefore be treated as drawing- and order-specific requirements rather than assumed product defaults.
Selesaikan Spesifikasi yang Bertentangan atau Tidak Ada Sebelum Pengukuran
Do not select a tolerance from memory, an old inspection sheet, or a generic catalog.
Place the punch on hold when:
- the drawing revision does not match the purchase order;
- the inspection report refers to another part or lot;
- the drawing and purchase specification contain conflicting limits;
- the material or coating designation is missing;
- the required datum or measurement method is unclear;
- an approved deviation is mentioned but not supplied.
Obtain written clarification from the responsible engineer, customer, or supplier before assigning a pass or fail result. The controlling-document hierarchy should follow the customer’s quality system or contract rather than an informal assumption.
Periksa Setiap Fitur Pukulan untuk Kerusakan yang Terlihat
Visual inspection is the fastest way to find obvious defects, but it should follow a consistent feature-by-feature sequence.
Use clean lighting and suitable magnification. Rotate the punch and inspect the complete circumference rather than viewing only one side.
| Zona inspeksi | Kondisi untuk diperiksa | Kemungkinan signifikansi | Tindakan umum berikutnya |
| Ujung tombak dan ujung | Terkelupas, retakan, pembulatan tepi, burr, deformasi, pengambilan | Loss of cutting quality, kelebihan beban lokal, dampak, memakai, adhesive material transfer | Ukuran, quarantine, regrind, or replace |
| Shank atau tubuh | Penilaian, menyebalkan, wear bands, korosi, cemas, material yang dipindahkan | Poor guidance, gesekan, ketidaksejajaran, lubrication problem, kecocokan yang salah | Bersih, measure diameter/runout, inspect mating parts |
| Kepala dan bahu | Jamur, peening, retakan, uneven seating marks, deformasi | Kelebihan beban, incorrect seating, retainer problem, dukungan yang tidak memadai | Karantina dan periksa kondisi retainer atau tempat duduk |
| Jari-jari transisi | retakan, grinding marks, abrupt surface changes | Konsentrasi stres, kerusakan penggilingan, fatigue initiation | Magnify, escalate, or replace |
| Permukaan berlapis | Peeling, mengelupas, goresan, perubahan warna, substrat terbuka | Coating damage, gesekan, dampak, korosi, memakai | Record location, assess function, seek engineering review |
| Tanda identifikasi | Missing or illegible part, lot, or serial information | Hilangnya ketertelusuran atau risiko revisi pencampuran | Tahan hingga identitas dikonfirmasi |
A small chip at the cutting edge is not equivalent to a superficial scratch on a non-working surface. The inspection record should state the defect location, approximate extent, and whether it affects a functional feature.
retakan, deformasi parah, or a damaged retention head generally justify immediate quarantine. Membelokkan, pengambilan, or one-sided scoring may require inspection of the die system as well as the punch. Detailed causes of cracking and catastrophic failure belong in the guide to kerusakan pukulan pada cetakan stamping.
Apa yang Tidak Dapat Dikonfirmasi oleh Inspeksi Visual
Visual inspection cannot reliably establish:
- exact body or tip diameter;
- overall or working length;
- kelurusan;
- kehabisan, konsentrisitas, or coaxiality;
- shaped-tip profile;
- numerical surface roughness;
- kelas material;
- heat-treatment conformity;
- kekerasan;
- coating identity.
A punch may look undamaged but still be dimensionally out of tolerance. Kelas bahan, kekerasan, and coating conformity may require traceable documentation or a specified test method.
Mengukur dimensi dan geometri yang mengontrol kesesuaian dan fungsi
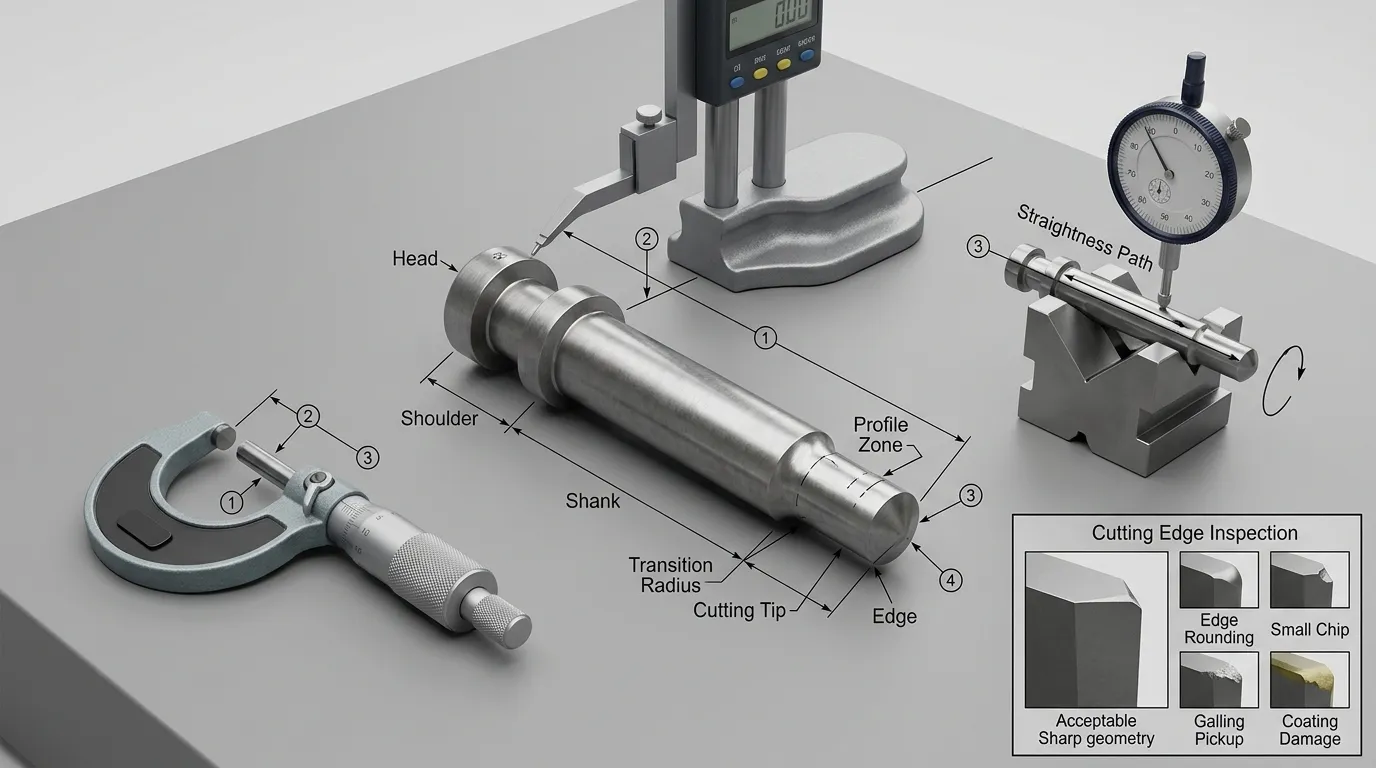
The approved drawing determines which dimensions and geometric controls must be inspected. Not every punch requires every measurement.
| Karakteristik | Mengapa itu penting | Metode pengukuran yang mungkin | Batasan yang signifikan | Sumber penerimaan |
| Diameter tubuh atau betis | Affects guidance, cocok, retensi, dan penyelarasan | Outside micrometer; suitable limit gauge | Lokasi kontak dan lancip harus dipertimbangkan | Spesifikasi gambar atau kesesuaian |
| Diameter ujung | Memengaruhi ukuran fitur yang ditusuk dan hubungan punch-die | Mikrometer, specialized gauge, optical system | Ujung kecil atau halus mungkin tidak sesuai dengan kontak standar | Menggambar |
| Profil ujung berbentuk | Mengontrol lubang non-bulat atau geometri yang terbentuk | Optical comparator, vision system, CMM | Membutuhkan penyelarasan datum dan interpretasi profil yang benar | Menggambar dengan persyaratan profil |
| Panjang keseluruhan | Supports identification, installation, and regrind tracking | Height gauge, micrometer, pembanding, dedicated fixture | Wajah tempat duduk harus bersih dan referensi secara konsisten | Menggambar |
| Panjang kerja atau proyeksi | Mempengaruhi posisi operasi dan penetrasi | Height gauge, pembanding, dedicated inspection fixture | Definition must match the drawing; do not borrow tablet-tooling terminology | Spesifikasi gambar atau pengaturan |
| Diameter dan ketebalan kepala | Memengaruhi retensi dan tempat duduk | Mikrometer, caliper for screening, pembanding | Gerinda atau kencing dapat mendistorsi kontak | Menggambar |
| Posisi bahu | Memengaruhi tempat duduk dan proyeksi rakitan | Height gauge, pembanding, CMM | Pengaturan datum harus mereproduksi persyaratan gambar | Menggambar |
| Kelurusan | Mendeteksi pembengkokan atau penyimpangan sumbu | Indicator with suitable support, CMM, dedicated fixture | Metode dukungan dan pilihan datum memengaruhi hasil | Batas layanan yang disetujui atau disetujui |
| Runout melingkar atau total | Menunjukkan variasi rotasi relatif terhadap sumbu datum | Indicator with centers or V-block; CMM | "Runout" harus cocok dengan kontrol gambar yang tepat | Menggambar |
| Konsentrisitas atau koaksialitas | Mengevaluasi hubungan antara sumbu atau fitur | CMM atau metode khusus yang disetujui | Jangan mengganti pemeriksaan runout sederhana kecuali teknik menyetujuinya | Menggambar |
| Tegak lurus | Memengaruhi tempat duduk atau keselarasan wajah ujung dan bahu | Indicator, surface plate setup, CMM | Memerlukan referensi datum yang valid | Menggambar |
| Kekasaran permukaan | Can influence friction, cocok, rilis, and galling | Penguji kekasaran permukaan | Parameter, batas, arah, and location must be specified | Gambar atau spesifikasi permukaan |
| Kekerasan | Dapat mengkonfirmasi persyaratan perlakuan panas | Uji kekerasan yang disetujui atau dokumentasi pemasok | Test scale, Lokasi, kondisi permukaan, and indentation effect matter | Gambar atau spesifikasi bahan |
Geometric terms should be interpreted according to the drawing standard in use. ISO 1101 defines geometrical tolerancing concepts in the ISO system, sementara ASME Y14.5 is widely used for US-oriented GD&T drawings.
A drawing that specifies runout should not be rewritten as concentricity during inspection. These controls describe different requirements and may require different measurement strategies.
SunshinePro’s tungsten-carbide punch page lists micrometer or caliper checks, projector measurement, and roughness testing for that product category. Those published methods show the types of inspection that may be relevant, but they do not prove that every punch or every order receives the same checks.
Pilih instrumen sesuai dengan toleransi dan fitur
Instrument choice should be based on the feature, toleransi, akses, and required measurement confidence.
| Instrumen | Penggunaan terbaik | Batasan utama |
| Mikrometer | Diameter dan ketebalan eksternal yang dapat diakses | Contact geometry may not suit small, meruncing, delicate, or irregular features |
| Kaliper | Identification, broad dimensions, and screening | Resolusi dan pengaruh operator mungkin tidak cocok untuk toleransi yang ketat |
| Pengukur ketinggian dan pelat permukaan | Axial dimensions, shoulder positions, and comparative height checks | Memerlukan tempat duduk dan pengaturan datum yang terkontrol |
| Indikator dial dengan V-block atau pusat | Runout, rotational variation, and some straightness checks | Hasil sangat bergantung pada posisi dukungan dan simulasi datum |
| Komparator optik atau sistem penglihatan | Profiles, sudut-sudut, jari-jari, tip shapes, and edge form | Requires alignment, magnification control, and correct profile interpretation |
| CMM | Geometri kompleks dan hubungan berbasis datum | Probe access, pemasangan, strategy, and uncertainty must be controlled |
| Pengukur pergi/tidak pergi | Verifikasi fungsional cepat dari batas ukuran | Memberikan informasi lulus/gagal tetapi bukan penyimpangan atau tren keausan yang sebenarnya |
| Penguji kekasaran | Verifikasi tekstur permukaan numerik | Requires the correct parameter, arah, batas, and measurement location |
Pengukur batas polos dicakup oleh ISO 1938-1. A go/no-go gauge can be efficient for repeated checks, but variable measurement is still useful when the actual size or rate of wear matters.
Surface-texture requirements should be read from the drawing rather than inferred from appearance. ISO 21920-1 covers the indication of profile surface texture in technical product documentation.
Putuskan apakah hasilnya dapat diterima
A measured value is not meaningful until it is compared with an approved requirement.
Possible acceptance sources include:
- the current approved drawing;
- the purchase specification;
- the control plan;
- an approved customer deviation;
- an approved sample with defined measurement criteria;
- a documented service limit;
- a validated internal wear limit.
Nominal size alone does not determine acceptance. A drawing dimension of 10 mm, misalnya, cannot be judged without its tolerance and any related geometric or surface requirements.
Use a controlled decision process:
| Kondisi hasil | Respons yang diperlukan |
| Jelas dalam persyaratan | Catat hasilnya dan terima atau kembalikan pukulan ke servis |
| Mendekati batas atau tidak konsisten | Verify cleanliness, suhu, instrumen, method, pemasangan, datum setup, and repeatability |
| Di luar persyaratan | Karantina pukulan dan mulai proses ketidaksesuaian yang disetujui |
| Spesifikasi hilang atau bertentangan | Tahan pukulan sampai klarifikasi tertulis diterima |
| Cacat berulang setelah penggantian atau penggilingan ulang | Selidiki sistem cetakan yang lebih luas dan kondisi proses |
Measurement uncertainty becomes important near a specification limit. ISO 14253-1 provides decision rules for proving conformity or nonconformity while accounting for measurement uncertainty.
In practical terms, a borderline reading should not be accepted or rejected casually. Confirm that the instrument and method are capable of resolving the requirement, then apply the organization’s documented decision rule.
Pengambilan sampel atau inspeksi 100% tergantung pada risiko dan persyaratan kontrak
The inspection quantity should be determined by:
- customer or contract requirements;
- characteristic criticality;
- lot size;
- supplier performance history;
- process capability;
- failure consequence;
- previous nonconformities;
- whether the result is needed for wear trending;
- the control plan.
A statement such as “100% inspected” should identify which characteristics were checked. It may mean every punch received an identification and visual check, while only selected pieces received complete dimensional inspection.
Go/no-go gauging may support rapid inspection of every piece, but it does not provide the variable data needed to evaluate size distribution or wear trends.
Gunakan Inspeksi Rutin untuk Melacak Keausan Sebelum Kegagalan
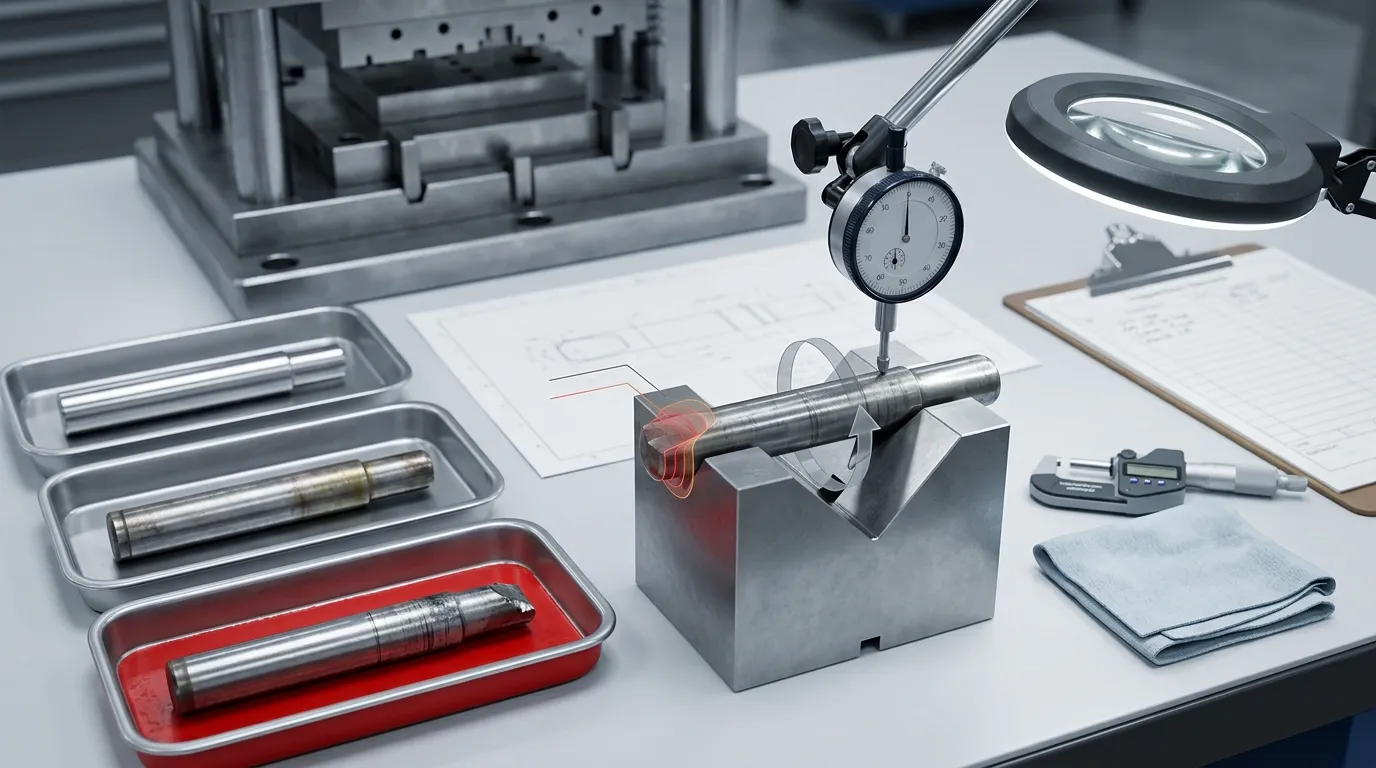
Routine QC should be based on risk and production history rather than one fixed interval for every punch.
Establish a baseline when the punch is first accepted, approved after setup, or returned from regrinding. Record dimensions and visible condition for the features most likely to change.
Trigger inspection when any of the following occurs:
- a planned production or maintenance interval is reached;
- the punch completes a high-risk or high-volume run;
- burr height or edge quality changes;
- stamped dimensions begin to drift;
- scratching or pickup appears on the part;
- stripping force increases;
- press load or operating sound changes;
- slug pulling or jamming occurs;
- a misfeed, tabrakan, or material double-feed occurs;
- a nearby punch chips or breaks;
- the tool is removed for maintenance;
- pelumasan, stock material, or process settings change;
- the punch returns from regrinding.
Compare current values with the baseline and approved service limits. Trend data can reveal gradual wear before a dimension crosses a rejection limit.
Production symptoms should be treated as inspection triggers, diagnosis tidak otomatis. Burrs may result from a worn punch, but they can also reflect die wear, pembersihan, penyelarasan, work-material variation, or stripper problems. Itu Panduan Cetakan Meninju provides broader context on die materials, toleransi, pembersihan, and system-level tooling considerations.
Verifikasi pukulan lagi setelah penggilingan ulang atau peristiwa abnormal
A sharp edge does not by itself prove that a reground punch is ready for service.
Setelah digiling ulang, periksa:
- cutting-edge form;
- burr-free condition;
- panjang keseluruhan;
- working length or projection;
- tip diameter or profile;
- surface damage or overheating;
- remaining regrind allowance, where documented;
- identification and regrind history.
After a collision, misfeed, jam, or nearby breakage, also check:
- retakan;
- permanent bending;
- head or shoulder deformation;
- kehabisan;
- permukaan tempat duduk;
- guide and retainer contact;
- the mating die opening and surrounding components.
Do not return a punch to service solely because no visible crack is present. A collision can change alignment or runout without producing an obvious surface defect.
Catat Hasilnya dan Tetapkan Disposisi Terkendali
Inspection records should identify the punch, the requirement, the method, the result, and the final decision.
Minimal, rekaman:
- nomor bagian;
- Nomor gambar dan revisi;
- pemasok;
- purchase order;
- lot or serial number;
- material and coating designation;
- inspection stage;
- characteristic inspected;
- specification and tolerance;
- measured result;
- instrument identification;
- inspector;
- inspection date;
- disposition;
- Catatan, photographs, or defect location where useful.
Use a controlled disposition rather than an informal “looks okay” decision.
| Menemukan | Tata Letak yang Mungkin |
| Semua karakteristik yang diperlukan sesuai | Terima atau kembali ke layanan |
| Hasilnya tidak konsisten atau mendekati batas | Bersih, stabilize, remeasure, or verify with a more capable method |
| Dokumentasi hilang | Tahan atau karantina sampai bukti diberikan |
| Keausan tepi yang dapat diperbaiki dalam tunjangan yang disetujui | Kirim untuk penggilingan ulang yang disetujui teknik |
| retak, severe chipping, permanent bending, or unsafe head damage | Ganti atau tolak |
| Dimensi berada di luar persyaratan | Karantina dan proses sebagai tidak sesuai |
| Kerusakan yang sama berulang kali | Investigate clearance, penyelarasan, panduan, retensi, pelumasan, dan kondisi proses |
Nonconforming punches should be clearly identified and physically segregated so they cannot return to production accidentally.
SunshinePro states that its quality approach includes raw-material inspection, pemantauan dalam proses, pengujian akhir, measuring equipment, and inspection reports. Buyers should still define the required inspection characteristics and documentation for each order rather than assume that one standard report fits every punch.
Apa yang Harus Diminta Dari Pemasok Punch Pin
A buyer should define inspection evidence before the order is released, especially for custom or critical punches.
Request the items that are relevant to the application:
- approved drawing and revision;
- part, lot, and serial identification requirements;
- drawing-specific inspection report;
- material certificate or certificate of conformity;
- heat-treatment or hardness evidence where specified;
- coating documentation where specified;
- penyimpangan yang disetujui;
- packing and corrosion-protection requirements;
- identification of characteristics receiving 100% inspection;
- identification of characteristics inspected by sampling;
- measurement method for tight or complex tolerances;
- traceability between the punch, certificate, and inspection report.
Broad catalog statements are not a substitute for characteristic-level evidence. A supplier may state a general tolerance capability, but the buyer still needs confirmation that the required feature, material, geometri, and measurement method are suitable for the specific drawing.
SunshinePro lists tool steel, baja berkecepatan tinggi, karbida, Pemesinan CNC, penggilingan presisi, EDM, perlakuan panas vakum, and drawing-based customization on its punch-related pages. These published options can support an RFQ discussion, but the exact material, proses, toleransi, pelapisan, and inspection documentation should be confirmed for the individual part.
Ringkasan Daftar Periksa Inspeksi Punch Pin
Use this condensed sequence for incoming, routine, post-regrind, and post-event inspections:
- Identify the inspection stage.
- Confirm the part number, lot or serial number, gambar, and revision.
- Review the purchase order, control plan, and document requirements.
- Inspect packaging and record transport damage.
- Clean the punch without damaging its edge or coating.
- Verify instrument condition, range, penyelesaian, and calibration status.
- Inspect the cutting edge, petunjuk, body, kepala, bahu, jari-jari, pelapisan, and identification.
- Measure the dimensions and geometric characteristics required by the drawing.
- Use an instrument suitable for the feature and tolerance.
- Compare results with the approved acceptance source.
- Verify borderline results and account for measurement uncertainty.
- Record the specification, result, instrumen, inspector, dan tanggal.
- Accept, hold, quarantine, regrind, mengganti, or reject through a controlled disposition.
- Investigate the wider die system when the same damage repeatedly returns.
For a custom or replacement punch, submit the approved drawing together with the required material, pelapisan, inspeksi, and documentation needs. SunshinePro The Punch Pin page provides its published product context, dan Halaman kontak can be used to request drawing review or clarify inspection-report requirements.
Bagikan:



Ditulis oleh Sunshine
di Sunshine, Kami adalah produsen dan pemasok profesional komponen cetakan presisi, menawarkan berbagai produk untuk aplikasi stamping dan cetakan injeksi. Fokus utama kami adalah mencetak cetakan, pin dan lengan ejector, serta tiang panduan dan bushing. Dengan pemesinan CNC canggih, kontrol kualitas ketat, dan kemampuan produksi yang kuat, kami memastikan keandalan, suku cadang presisi tinggi, bersama dengan komponen standar yang tersedia untuk pasokan global yang cepat dan efisien.
BERITA
DAPATKAN LAYANAN
Dengan suku cadang berkualitas untuk memenuhi setiap anggaran dan staf ramah yang terlatih untuk membuat kunjungan Anda menjadi informatif dan tanpa repot.
