



Inspeksi Keausan Pin Batas Cetakan: Pengukuran dan Petunjuk Kegagalan
A proper mold limit pin wear inspection combines visual evidence with controlled dimensional measurements. A polished contact face alone does not prove that the pin is damaged, while a pin that appears clean may still have lost diameter, effective height, or straightness.
The pin should be compared with a controlled drawing, an approved inspection record, a qualified spare, or a documented historical baseline. There is no universal wear allowance or replacement cycle that applies to every mold.
Pin batas adalah salah satu bagian dari sistem yang lebih luas yang dapat diganti Bagian standar cetakan (disimpulkan). This guide focuses only on how to inspect their wear, interpret failure clues, and document the next technical action.
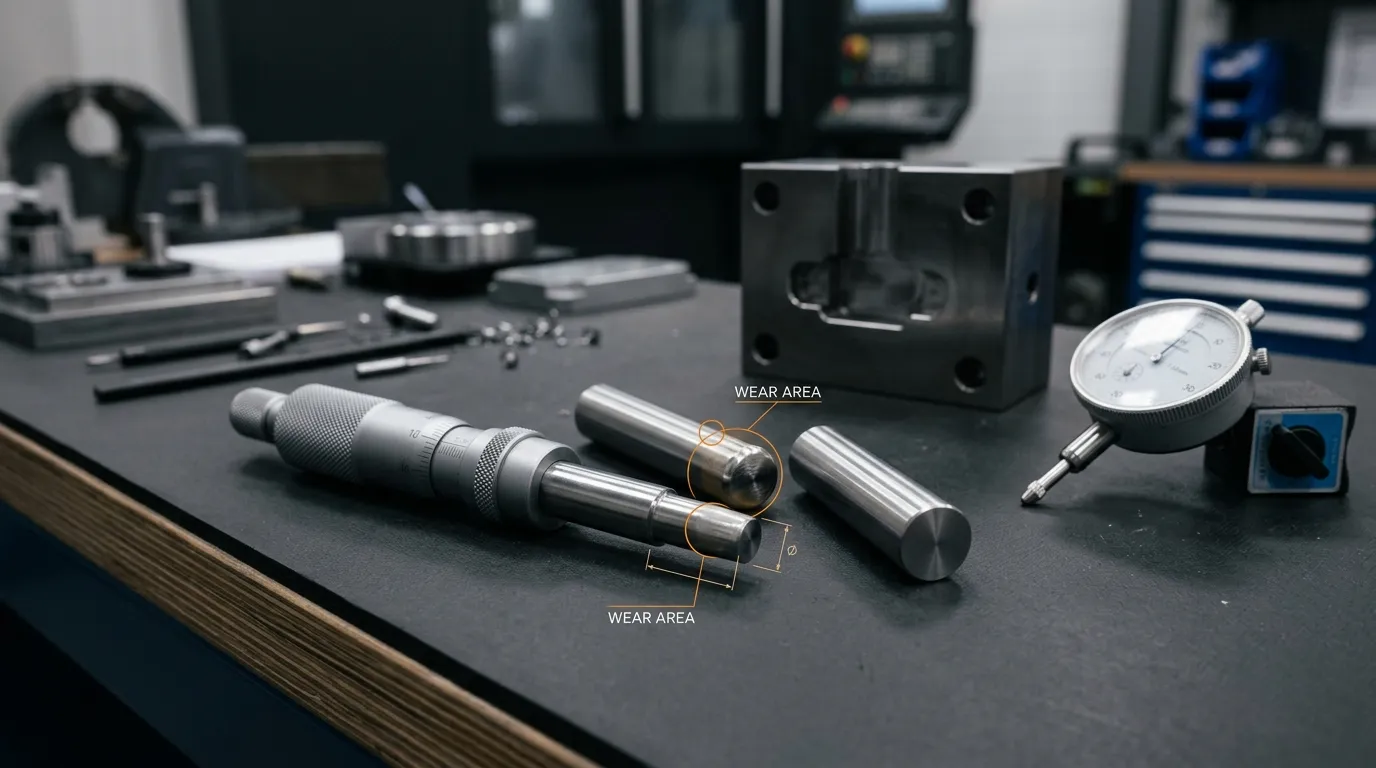
Tetapkan Referensi Inspeksi yang Aman dan Valid
Before opening, removing, or measuring a limit pin, isolate the molding machine and control all stored energy according to the procedures that apply at the facility. Stored hydraulic pressure, mata air, suspended mold sections, gravity, and moving plates can remain hazardous even after the machine has stopped.
Untuk tempat kerja di AS, OSHA 29 CFR 1910.147 provides requirements for controlling hazardous energy during servicing and maintenance. Other countries and regions have their own requirements, so the applicable local procedure must control the work.
Before measurement:
- Support the mold and any movable assembly securely.
- Record the pin’s position before removal.
- Photograph visible damage before cleaning it away.
- Remove oil, loose debris, corrosion residue, and dirt from measuring surfaces.
- Check for burrs that could distort the reading.
- Allow the pin and reference equipment to reach a stable measurement condition.
- Confirm which drawing revision or baseline will be used.
Confirm the Pin by Function, Not Name Alone
Persyaratan Pin Batas, pin berhenti, dan pin penghenti may describe similar travel-limiting functions, but naming is not consistent across mold designs and suppliers.
Identify the component by asking:
- Which plate or assembly does it stop?
- Where is its contact face?
- Which surface does it contact at the end of movement?
- Does it carry stopping load, guide movement, return a plate, eject a part, or locate an assembly?
A return pin, pin ejektor, pin panduan, dowel, or locating pin should not be assessed using a limit-pin procedure simply because it has a similar cylindrical shape.
Pilih Referensi Sebelum Melakukan Pengukuran
A measured value has little meaning until it is compared with a valid requirement. Use the strongest available reference in this order:
- Gambar komponen atau cetakan yang dikendalikan
- Spesifikasi OEM atau standar inspeksi yang disetujui
- Laporan inspeksi yang disetujui sebelumnya
- Cadangan baru yang memenuhi syarat
- Pengukuran historis dari posisi pin yang sama
- Perbandingan relatif dengan pin yang cocok dari rakitan yang sama
Confirm the units, datum surfaces, toleransi, and drawing revision. A nominal length measured from the wrong shoulder or reference face may produce a precise but useless result.
When a result is close to an acceptance limit, measurement uncertainty also matters. ISO 14253-1:2017 addresses how specification limits and measurement uncertainty affect conformity decisions.
Manufacturing tolerances listed on a supplier’s product page should not automatically be treated as service-wear limits. New-part acceptance and continued-service acceptance are different engineering decisions.
Periksa pin dan sistem kontaknya sebelum mengukur
Begin with a systematic visual examination. Use strong lighting and magnification where needed, but inspect the surrounding components as well as the pin itself.
Check these areas:
- Kontak atau hentikan wajah
- Tepi luar permukaan berhenti
- Betis silinder
- Transisi diameter
- Bahu atau kepala
- Fitur utas dan retensi
- Permukaan tempat duduk
- Permukaan berhenti yang sesuai dalam cetakan
- Pin lain yang berbagi beban berhenti yang sama
Look for polishing, flattened areas, mushrooming, penilaian, metal transfer, memotong lubang, korosi, retakan, chipped edges, kerusakan benang, and fretting around retained interfaces.
The mating stop surface deserves equal attention. An indentation, burr, embedded particle, or worn pocket can change the functional stopping position even when the pin itself remains close to its original length.
Pisahkan Pemolesan Saksi Normal dari Kerusakan Abnormal
A centered and stable polished witness mark may simply show where normal contact occurs. It becomes more concerning when the pattern changes shape, moves toward one edge, or differs significantly between pins in the same set.
| Pengamatan | Interpretasi awal |
|---|---|
| Centered, even polishing | Dapat mengindikasikan kontak normal dan seimbang |
| Tanda satu sisi atau diagonal | Possible misalignment, unequal height, atau beban samping |
| Permukaan berhenti pipih | Benturan berulang atau beban terkonsentrasi |
| Tepi jamur | Deformasi plastik pada permukaan kontak |
| Penilaian longitudinal | Abrasive debris, kontak geser, atau ketidakselarasan |
| Logam atau pickup yang diolesi | Kemungkinan keausan atau perekat |
| Retak atau tepi terkelupas | Kerusakan struktural yang membutuhkan eskalasi segera |
| Karat atau lubang | Kehilangan material terkait korosi atau kondisi penyimpanan yang buruk |
These observations are clues, not final diagnoses. Keausan satu sisi, misalnya, may come from a bent pin, unequal pin heights, keausan sistem panduan, a damaged seat, or an uneven mating surface.
Measure Diameter Wear, Taper, and Ovality
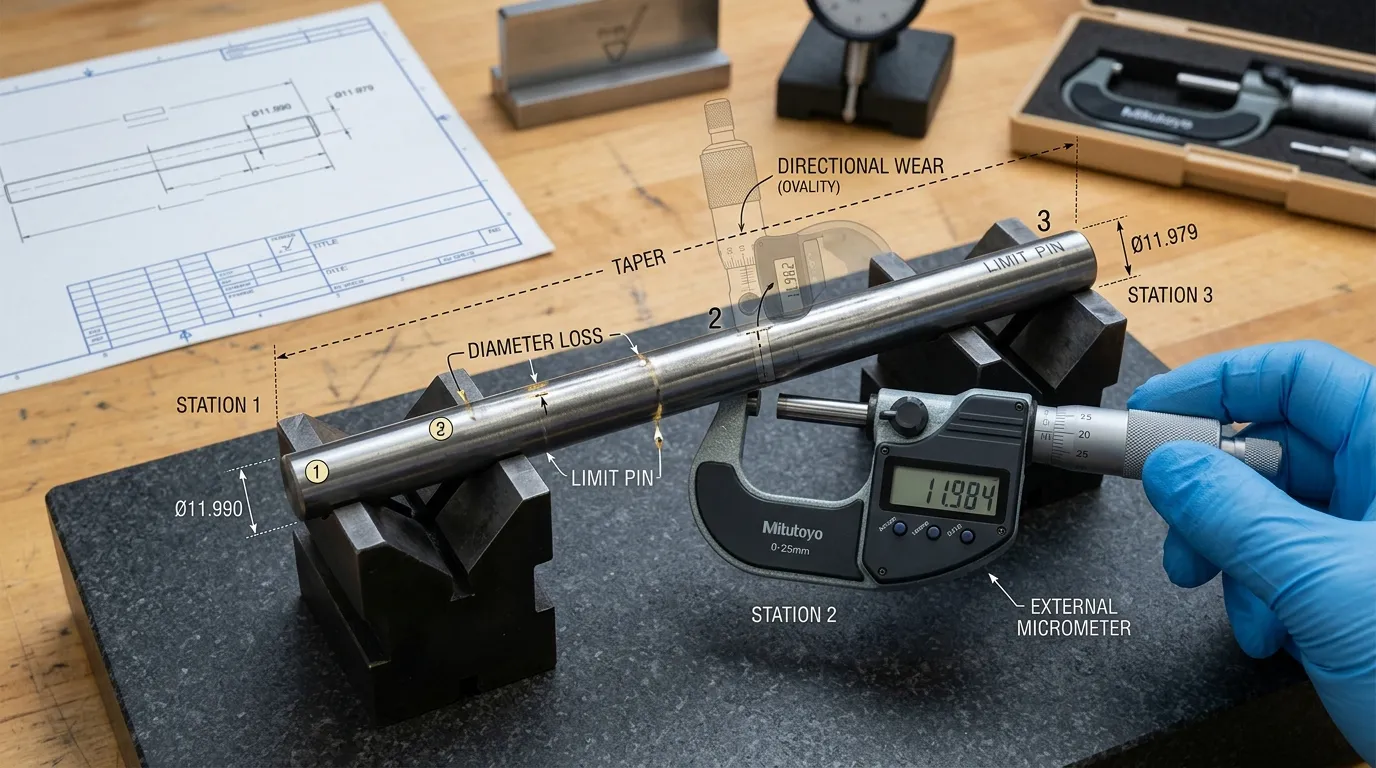
A single diameter reading cannot describe the complete wear condition of a limit pin. Measurements should be taken at repeatable axial locations and in more than one rotational orientation.
An external micrometer is usually more suitable than a caliper when small diameter changes must be evaluated. ISO 3611:2023 defines design and metrological characteristics for external micrometers. Calipers are useful for preliminary checks, but their capability must match the tolerance and expected amount of wear. Their general metrological characteristics are covered by ISO 13385-1:2019.
A practical measurement sequence is:
- Mark the measurement locations along the shank.
- Measure near the upper working area.
- Measure near the centre.
- Measure near the lower working area or seat, where accessible.
- At each location, take readings in at least two rotational orientations.
- Record the position and orientation of every reading.
- Compare the results with the drawing, spare, baseline, and corresponding pins.
This pattern helps separate several conditions:
- Diameter loss: The measured diameter is smaller than the approved reference.
- Taper: Diameter changes progressively along the pin’s length.
- Ovalitas: Readings differ when the pin is rotated at the same axial position.
- Pakaian lokal: One short area shows greater loss than the rest of the shank.
Directional diameter loss often supports an investigation into side loading or alignment. Progressive axial wear may indicate contact in a specific working zone rather than uniform material loss.
Do not assign a universal rejection value. The acceptable difference depends on the controlled design, cocok, muatan, and function of the individual mold.
Check Length, Protrusion, and Effective Stop Height
Overall length is not always the most important axial measurement. The functional dimension may be free length, installed protrusion, shoulder-to-face distance, recess depth, or assembled stop height.
First identify the dimension that actually controls plate movement. Then check:
- Panjang keseluruhan atau bebas
- Deformasi wajah kontak
- Tonjolan terpasang
- Tempat duduk bahu
- Keterlibatan utas
- Kedalaman kursi
- Kondisi permukaan kawin
- Tinggi relatif pin yang cocok
A pin may measure correctly after removal but still sit too low because of debris under the shoulder, kerusakan benang, seat wear, or an incorrect replacement geometry. The opposite can also occur: the pin may appear shortened when the real loss is an indentation in the opposing stop surface.
Use a height gauge, depth micrometer, height micrometer, or another suitable setup based on the controlled datum and accessibility. The setup must be rigid enough to produce repeatable results.
Bandingkan semua pin yang berbagi beban berhenti
Several limit pins may work together to stop the same moving plate. Their effective heights should be compared because one high pin can contact first and carry more load than the others.
Periksa apakah:
- Contact patterns appear on all corresponding pins.
- Protrusion or effective height is consistent.
- One pin has a larger polished or deformed area.
- One position shows deeper indentation on the mating surface.
- A previously replaced pin differs from the remaining set.
- One pin contacts before the plate becomes parallel.
Replacing only the visibly damaged pin may not solve the problem if the set has unequal heights or if another component caused the load imbalance.
Check Runout, Membungkuk, and Straightness
A pin subjected to side loading, collision, or severe misalignment may bend without showing major diameter loss.
Where the geometry permits, support the clean pin on suitable datum surfaces or V-blocks and use a dial indicator to measure variation during rotation. Record the indicator position and support arrangement so the test can be repeated.
Before accepting the result, memeriksa:
- Gerinda di bawah titik support
- Kotoran pada blok-V
- Permukaan silinder rusak
- Bahu tidak teratur
- Penyelarasan indikator yang buruk
- Gaya pengukur yang berlebihan
- Pergerakan perlengkapan penyangga
Runout, kelurusan, and coaxiality are related but not interchangeable terms. ISO 1101:2017 provides the geometrical tolerancing framework for form, orientasi, Lokasi, dan kehabisan. Straightness terminology is further defined in ISO 12780-1:2011.
The total indicated variation from a workshop setup should not automatically be treated as the drawing’s straightness error. It is an inspection result that must be interpreted against the specified geometry and measurement method.
When bending or directional wear is found, inspect the mold’s alignment system. Worn pin cetakan dan bushing can allow plate movement that places abnormal side load on a limit pin.
Menafsirkan Pola Keausan Tanpa Melompat ke Akar Penyebab
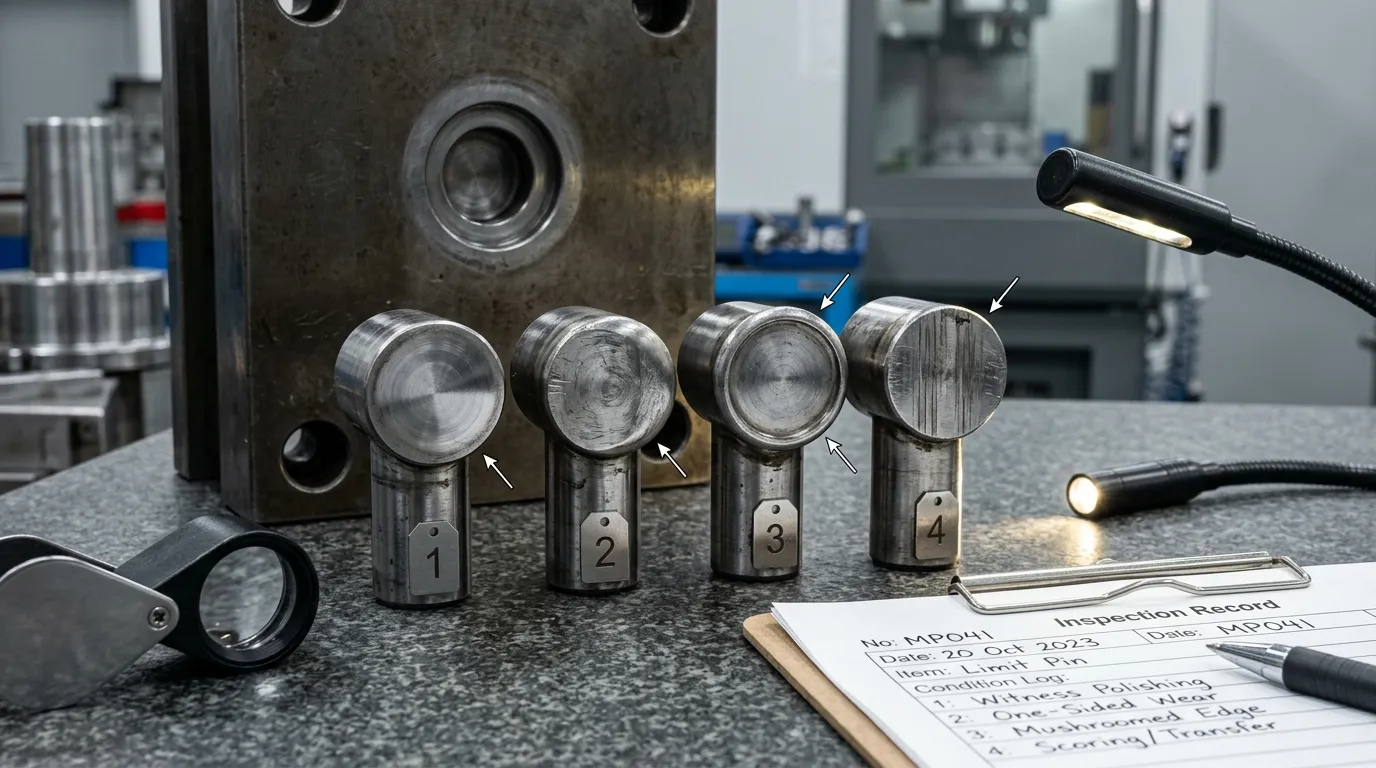
Use each wear pattern to guide further inspection rather than treating it as proof.
| Petunjuk kegagalan | Kemungkinan penyebab | Pemeriksaan konfirmasi | Respon segera |
| Tanda saksi satu sisi | Ketidaksejajaran, unequal pin height, angled mating surface | Compare matched-pin heights, guide condition, paralelisme lempeng | Lanjutkan diagnosis sebelum mengganti pin |
| Wajah pipih atau jamur | Dampak berulang, overtravel, insufficient contact area, unequal loading | Check effective height, stroke, mating surface, other pins | Mengukur kehilangan aksial dan eskalasi jika deformasi aktif |
| Penilaian longitudinal | Puing-puing, keausan abrasif, kontak geser, penyelarasan yang buruk | Inspect bore or surrounding surface, Kontaminasi, sistem panduan | Hapus kontaminasi dan nilai kehilangan diameter |
| Galling atau transfer logam | High friction, keausan perekat, poor surface compatibility | Look for transferred material, heat discoloration, rough mating surface | Hentikan kerusakan berkelanjutan dan selidiki pasangan kontak |
| Kehilangan diameter lokal | Keausan kontak atau abrasif terkonsentrasi | Diameter peta pada beberapa posisi aksial | Bandingkan dengan gambar dan data historis |
| Lancip atau ovalitas | Directional wear, beban samping, uneven support | Rotate measurements, inspect alignment and seating | Tentukan apakah keausan stabil atau berkembang |
| Runout yang berlebihan | Membungkuk, collision, pemuatan samping | Repeat indicator setup, inspect guide system and plate movement | Tinjauan teknik sebelum digunakan kembali |
| Lubang atau korosi | Kelembapan, paparan kimia, poor storage | Periksa komponen terdekat dan kondisi penyimpanan | Menilai kedalaman dan efek struktural |
| Retak atau tepi terkelupas | Impact fatigue, kelebihan beban, material damage | Periksa dengan pembesaran yang sesuai atau metode NDT yang disetujui | Hapus dari layanan dan eskalasi |
| Kerusakan benang atau bahu | Loosening, improper seating, repeated movement | Check seat, pertunangan, retention and installed height | Perbaiki masalah retensi sebelum penggantian |
Abnormal sound, menempel, plate travel changes, kilatan, or mismatch can justify an unscheduled inspection. They do not independently prove that the limit pin is the failed component.
Decide Whether to Continue, Memantau, Mengganti, or Escalate
The final decision should combine dimensional results, visible condition, functional evidence, and the approved acceptance criteria.
| Keputusan | Kondisi yang sesuai |
| Lanjutkan dalam layanan | Measurements meet approved criteria, contact is stable, no structural damage is present, and associated components are acceptable |
| Memantau | Minor measurable change is permitted, the condition is stable, and a documented reinspection plan is approved |
| Mengganti | The pin is outside its controlled specification, has unacceptable height variation, deformasi parah, damaged retention features, retak, mengelupas, or active galling |
| Tinjauan teknik | No valid specification exists, results conflict, uncertainty is too high, damage keeps returning, or system-level misalignment is suspected |
A pin should not be polished or reground automatically. Material removal can change its effective length, stop height, waktu kontak, dan distribusi beban. Serviceability depends on the component’s function and approved dimensional limits.
Generic cycle-count recommendations are also unreliable. Two molds using similar pins may create very different impact loads, alignment conditions, contamination exposure, and maintenance histories.
Catat Inspeksi dan Hindari Kesalahan Pengukuran Umum
A useful inspection record should include:
- Identifikasi cetakan
- Posisi pin
- Nomor gambar dan revisi
- Referensi yang digunakan
- Instrumen pengukuran dan resolusi
- Lokasi pengukuran
- Nilai dan satuan yang direkam
- Foto
- Kondisi permukaan kawin
- Kondisi pin yang cocok
- Gejala operasi yang relevan
- Disposisi akhir
- Pemicu inspeksi ulang atau interval yang disetujui
Consistent records make it possible to see whether wear is stable or accelerating.
Common errors include:
- Measuring through oil, Ketenangan, dirt, or burrs
- Mengukur komponen panas terhadap data referensi suhu ruangan
- Hanya mengambil satu pembacaan diameter
- Mengubah lokasi pengukuran di antara inspeksi
- Menggunakan kaliper di mana resolusi yang lebih besar diperlukan
- Runout yang diindikasikan membingungkan dengan kelurusan yang ditentukan gambar
- Mengabaikan kursi atau permukaan penghenti kawin
- Membandingkan pin yang tidak cocok secara fungsional
- Menghilangkan kerusakan sebelum memotretnya
- Memperlakukan toleransi manufaktur suku cadang baru sebagai batas keausan servis
Broader tolerance, baja, and inspection considerations for Bagian cetakan presisi can support replacement planning, but the used pin must still be judged against its own controlled requirements.
Menyiapkan data yang diperlukan untuk pengganti atau pin kustom
When inspection confirms that a replacement is required, prepare enough information to reproduce the functional geometry rather than sending only the worn component’s current dimensions.
Menyediakan:
- Menggambar terkontrol atau sketsa berdimensi
- Dimensi nominal
- Dimensi aus terukur
- Tinggi berhenti fungsional
- Geometri wajah kontak
- bahu, kepala, benang, and seat details
- Material and hardness requirement, where known
- Kuantitas
- Persyaratan yang ditetapkan yang cocok
- Foto pin dan permukaan kawin
- Hasil inspeksi
- Kemungkinan penyebab kegagalan
- Dokumentasi inspeksi yang diperlukan
SunshinePro mencantumkan standar dan non-standar pin batas cetakan options, including customization from dimensional requirements. Its published product information identifies S45C/45# steel, penggilingan presisi, threaded construction, perlakuan panas vakum, and a stated hardness of 15–17 HRC for that listed product.
Those details are product-specific. They should not be assumed to apply to every existing pin or used as universal replacement criteria.
Replacing the pin without correcting damaged seating, an indented stop surface, unequal matched heights, or alignment problems can cause the new component to fail in the same way. After the cause and required geometry are documented, the drawing, pengukuran, and photographs can be submitted through SunshinePro’s Halaman kontak for a standard or custom replacement discussion.
Bagikan:



Ditulis oleh Sunshine
di Sunshine, Kami adalah produsen dan pemasok profesional komponen cetakan presisi, menawarkan berbagai produk untuk aplikasi stamping dan cetakan injeksi. Fokus utama kami adalah mencetak cetakan, pin dan lengan ejector, serta tiang panduan dan bushing. Dengan pemesinan CNC canggih, kontrol kualitas ketat, dan kemampuan produksi yang kuat, kami memastikan keandalan, suku cadang presisi tinggi, bersama dengan komponen standar yang tersedia untuk pasokan global yang cepat dan efisien.
BERITA
DAPATKAN LAYANAN
Dengan suku cadang berkualitas untuk memenuhi setiap anggaran dan staf ramah yang terlatih untuk membuat kunjungan Anda menjadi informatif dan tanpa repot.
