



Pilihan Produsen Pin Batas Cetakan: Daftar Periksa Kapabilitas
Mold limit pin manufacturer selection should begin with the part’s function and drawing—not the supplier’s price, factory age, equipment list, or certification logos. A capable supplier must be able to produce the required geometry, control the specified material and hardness, measure the critical characteristics, document conformity, and repeat the approved result in later orders.
Keputusan pertama adalah apakah aplikasi dapat menggunakan stok Bagian standar cetakan (disimpulkan) or requires a custom limit pin made from a drawing or sample. Standard and custom parts need different levels of supplier qualification, but neither should be approved on marketing claims alone.
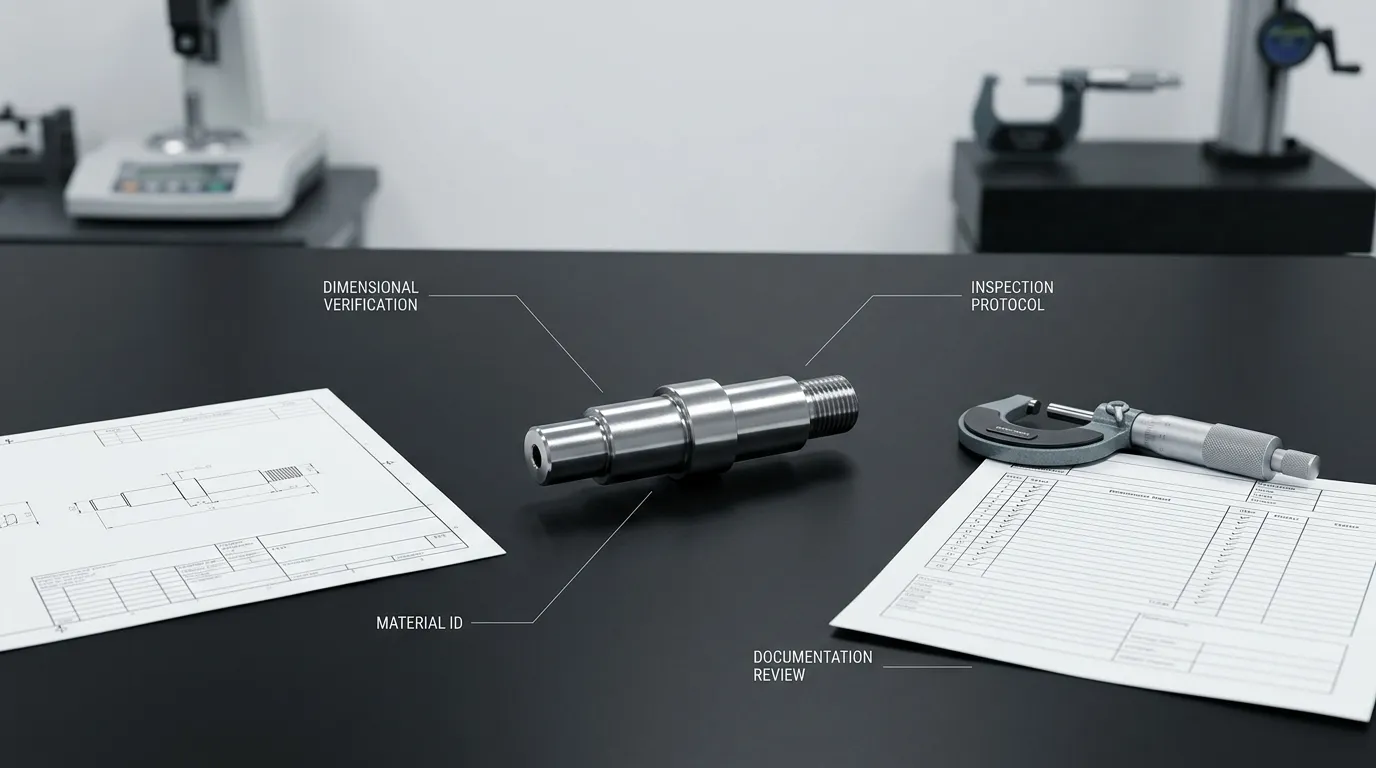
Tentukan persyaratan pin batas sebelum membandingkan produsen
A manufacturer cannot confirm capability until the buyer defines what the limit pin must do. The same general part name may refer to components used to stop movement, limit a stroke, retain an assembly, or support a positioning function. Each use creates different critical dimensions and risks.
Start by confirming:
- what movement the pin controls;
- where the load acts;
- whether the pin receives repeated impact;
- how it seats or mounts;
- whether it has a shoulder, kepala, langkah, benang, chamfer, or radius;
- which dimensions affect the final stopping position;
- whether the part is for a new mold, a replacement, or a modified mechanism;
- which characteristics are mandatory for function and interchangeability.
This distinction also prevents confusion between limit pins and other cylindrical mold components. Pin panduan, pin ejector, return pins, dowels, and core pins may look similar, but their operating conditions and acceptance requirements can be different. Broader alignment, pembersihan, and wear considerations are covered separately in the guide to pin cetakan dan bushing.
Konfirmasikan apa yang sebenarnya dikendalikan oleh pin
The supplier should not be asked to quote from a part name alone. A drawing, assembly view, physical sample, or clear application description should show the pin’s intended function.
Misalnya, a dimension controlling the mold’s stopping position may need closer attention than a non-functional relief feature. A threaded section may affect retention, while a shoulder face may determine seating. If impact occurs at one end, the material condition, heat-treatment route, end geometry, and inspection priorities may also change.
The buyer should identify these critical-to-quality characteristics before sending the RFQ. Selain itu, the supplier may quote a technically manufacturable part that does not address the actual functional risk.
Putuskan apakah persyaratan tersebut standar atau kustom
| Jalur sumber | Cocok ketika | Fokus kualifikasi |
|---|---|---|
| Pin batas standar atau stok | The supplier’s published dimensions, material, kekerasan, and geometry match the requirement | Confirm the exact catalog specification, stock status, keterlacakan, dan konsistensi penggantian |
| Pin standar yang dimodifikasi | Bagian dasar standar membutuhkan pemesinan terbatas atau perubahan fitur | Confirm which original characteristics remain controlled and how modification affects hardness, menyelesaikan, or geometry |
| Pin batas sepenuhnya kustom | The drawing specifies non-standard dimensions, toleransi, material, kekerasan, benang-benang, bahu, or finish | Conduct drawing review, process review, persetujuan sampel, dimensional verification, and repeat-order control |
A stocked part can reduce qualification work only when its documented specification matches the application. A custom part needs stronger drawing control because the approved dimensions and process route become the basis for future orders.
Siapkan Paket RFQ Pin Limit Lengkap
A vague RFQ produces vague capability claims and quotations that are difficult to compare. The manufacturer should receive enough information to review feasibility, choose a suitable process route, identify inspection requirements, and disclose any exceptions.
A useful RFQ package should include:
Informasi teknis
- revision-controlled 2D drawing;
- 3D CAD model when the geometry is difficult to interpret from the drawing;
- nominal dimensions and tolerances;
- datum references and geometric controls where functionally necessary;
- material grade and required condition;
- hardness or heat-treatment requirement;
- surface-texture requirement where relevant;
- thread standard, ukuran, kelas, depth, and inspection requirement;
- coating or surface-treatment requirement, jika berlaku;
- approved reference sample when a drawing is incomplete.
Informasi pesanan
- prototype or sample quantity;
- kuantitas produksi;
- expected repeat-order pattern;
- annual or forecast demand where available;
- required delivery destination;
- preferred shipping terms;
- required packaging and identification.
Informasi kualitas
- dimensions requiring actual measured values;
- material-document requirements;
- heat-treatment-document requirements;
- sample or first-article expectations;
- required conformity documents;
- traceability requirements;
- treatment of deviations or substitutions;
- record-retention expectations.
The drawing should remain the controlling technical document. Prinsip-prinsip dalam ASME Y14.5 support clear communication of dimensions, toleransi, tanggal, and geometric relationships. The supplier should not be expected to infer missing functional requirements from a model or sample alone.
SunshinePro describes a workflow that begins with consultation and drawing submission, followed by review and quotation. Nya Halaman Produk Pin Batas Cetakan can provide initial product context, but the buyer’s released drawing and agreed quotation should define a custom order.
Periksa kemampuan manufaktur yang memengaruhi kesesuaian pin batas
The correct manufacturing capability depends on the pin’s geometry and specification. A long equipment list is less useful than a clear explanation of how each critical feature will be produced, finished, and inspected.
The supplier should be able to connect the drawing to a realistic process sequence.
| Batasi persyaratan pin | Kemampuan untuk memverifikasi | Bukti untuk diminta |
| Diameter luar yang dikendalikan | Turning and, jika diperlukan, final precision grinding | Penjelasan proses dan hasil dimensi |
| Geometri berundak atau bahu | Stable turning, setup control, and feature relationship control | Sampel yang sebanding atau laporan artikel pertama |
| Fitur berulir | Metode produksi dan inspeksi benang yang sesuai | Konfirmasi spesifikasi ulir dan hasil inspeksi |
| Kekerasan yang ditentukan | Rute perlakuan panas terkontrol dan pengujian kekerasan | Catatan perawatan dan hasil kekerasan jika diperlukan |
| Hubungan geometris yang ketat | Suitable workholding, urutan pemesinan, and measurement method | Rencana inspeksi khusus gambar |
| Tekstur permukaan yang terkontrol | Proses finishing yang sesuai dan pengukuran profil jika ditentukan | Hasil dan metode tekstur permukaan |
| Pertukaran pesanan berulang | Revision control, process consistency, and retained approval records | Perjanjian penggambar dan kontrol perubahan yang disetujui |
Cocokkan geometri dengan proses produksi
A simple cylindrical pin may need turning followed by grinding. A stepped, berbahu, or threaded part may require several setups and a defined sequence to maintain relationships between features.
Questions for the manufacturer should include:
- Which features will be turned, ground, threaded, or finished by another method?
- Is the final diameter established before or after heat treatment?
- How will shoulders and end faces be held relative to the main diameter?
- How will thread concentricity or alignment be checked when it affects assembly?
- Will the production sample use the same process route planned for repeat orders?
- Which dimensions are expected to change during heat treatment?
- How much finishing allowance is retained for final grinding?
The answers should relate directly to the drawing. Claims such as “high precision,” “advanced machining,” or “tight tolerance capability” are not enough without a process explanation and inspection evidence.
Verify Material, Perlakuan Panas, and Grinding Control
Bahan, perlakuan panas, and final grinding are connected. The material grade affects machinability and the available treatment route. Heat treatment can change hardness but may also introduce distortion. Final grinding may then be required to restore the specified diameter, geometric condition, or surface.
The supplier should confirm:
- the exact material designation;
- how incoming material is identified;
- whether a material certificate is available when required;
- the specified heat-treatment condition;
- the required hardness scale and test location;
- whether heat treatment is internal or subcontracted;
- how treatment batches are linked to finished parts;
- when final grinding occurs;
- how grinding burn, pergeseran dimensi, or surface damage is controlled;
- how the finished condition is verified.
SunshinePro’s product page lists S45C for its displayed mold limit pin and describes outer-diameter precision grinding and vacuum heat treatment. Those statements may support an initial capability discussion, but they do not establish that the same material, kekerasan, or process is suitable for every custom application.
Where Rockwell hardness is specified, the test method should be appropriate to the material, ketebalan, permukaan, and required scale. ISO 6508-1 provides the standardized method for Rockwell hardness testing of metallic materials.
Broader considerations involving steel, menyelesaikan, toleransi, and quality inspection are addressed in the guide to Bagian cetakan presisi.
Identifikasi Proses Penting Mana yang Dialihdayakan
Outsourcing is not automatically a disqualification. The risk comes from undisclosed or poorly controlled outsourcing.
Ask the prospective supplier:
- Which operations are performed at its own facility?
- Which operations are subcontracted?
- How are subcontractors approved?
- How are material and heat-treatment records linked to the finished batch?
- Who is responsible for final inspection?
- Will the buyer be notified before a critical process or subcontractor changes?
- What happens if the external processor causes a delay or nonconformance?
A supplier that controls an approved heat-treatment source and accepts full responsibility for conformity may present less risk than a supplier that claims everything is internal but cannot provide clear records.
Verify Measurement Capability, Not Just Claimed Tolerances
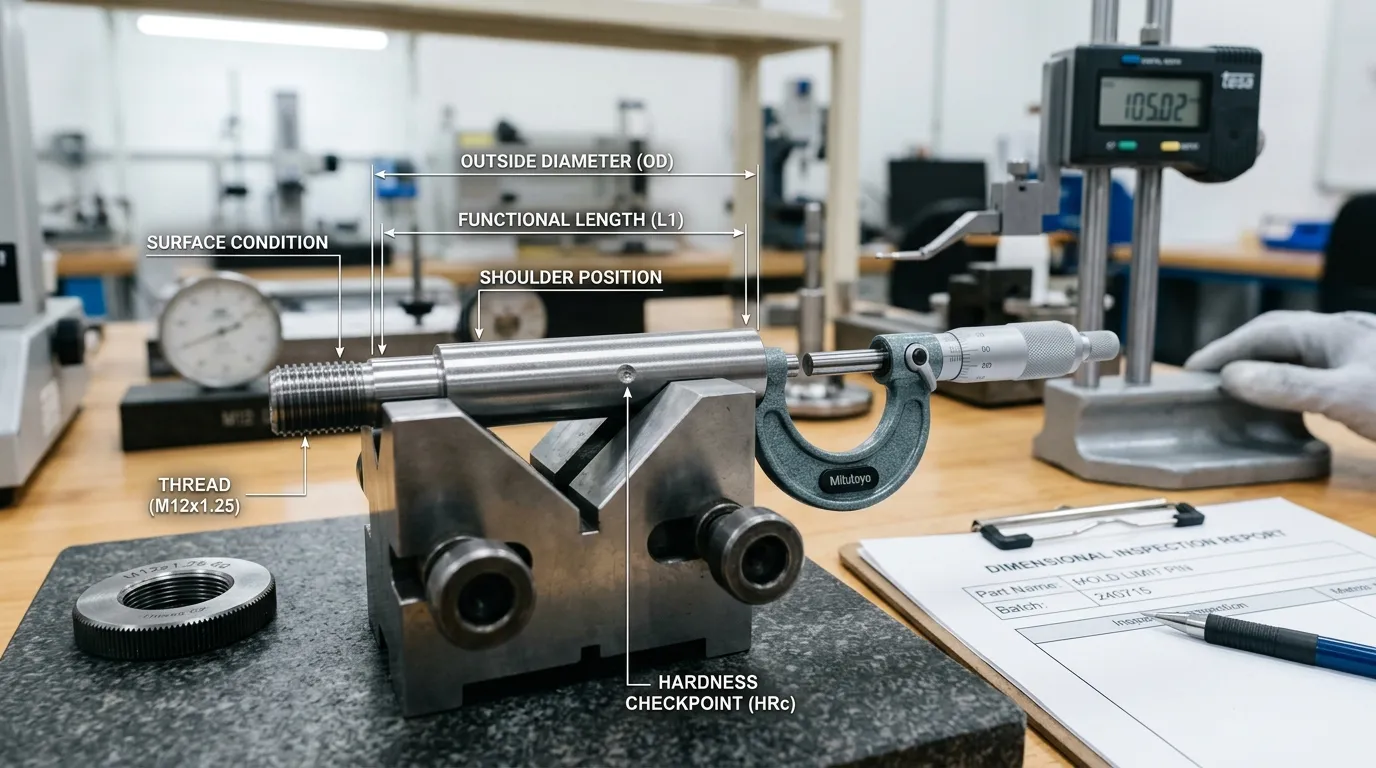
Manufacturing a dimension and measuring it reliably are separate capabilities. A supplier may say it can hold a tolerance, but the buyer still needs to know how that characteristic will be checked.
The measurement method should suit the feature, toleransi, accessibility, and required confidence.
| Karakteristik | Metode inspeksi yang mungkin | Titik verifikasi pembeli |
| Diameter luar yang dapat diakses | Mikrometer atau instrumen dimensi lain yang sesuai | Range, resolution, calibration, lokasi pengukuran, and actual result |
| Panjang atau posisi bahu | Height measurement, comparator, CMM, or suitable fixture | Pengaturan dan pengulangan datum |
| Hubungan geometris | CMM atau metode lain yang divalidasi | Equipment suitability, program, fixture, and reported result |
| Benang | Thread gauge, optical method, or other suitable inspection | Standar, kelas, depth, and acceptance method |
| Kekerasan | Penguji kekerasan yang sesuai | Skala, test location, persiapan permukaan, and result |
| Tekstur permukaan | Instrumen tekstur permukaan berbasis profil | Parameter, evaluation conditions, direction, and result |
The table does not prescribe one instrument for every supplier. A micrometer may be more appropriate than a CMM for an accessible external diameter, while a CMM or comparator may be useful for geometric relationships or profile features. The method should be selected from the actual drawing requirement.
A useful report should identify:
- the drawing characteristic;
- nominal value or specification;
- tolerance or acceptance limit;
- actual measured result;
- inspection status;
- measurement method or instrument where required;
- sample or batch identification;
- revisi gambar.
ASME Y14.45 establishes practices for reporting measurement data associated with dimensional specifications. ISO 10012 addresses measurement-management systems and the control needed to support reliable measurement results.
SunshinePro states that its workflow includes initial material inspection, inspeksi dalam proses, dan inspeksi akhir. Buyers should still confirm which characteristics are checked, which instruments are used, what records are supplied, and whether actual measured values are available for their order.
Minta Bukti Sebelum Memilih Produsen
A supplier should be evaluated on evidence that matches the project risk. Not every order needs the same document package, but critical custom parts require more than a quotation and a verbal tolerance confirmation.
Possible prequalification evidence includes:
- a redacted dimensional report for a comparable part;
- a sample material certificate;
- a heat-treatment record;
- a process-flow summary;
- identification of outsourced processes;
- calibration or measurement-control information;
- a current quality-management certificate where relevant;
- nonconformance and corrective-action procedures;
- drawing-revision and engineering-change controls;
- sample packaging and identification method.
A quality-management certificate can support confidence in the supplier’s documented system, but it does not prove that the company can produce one specific limit pin. The certificate holder, facility, scope, issuing body, and validity should be checked. Official Panduan sertifikasi ISO distinguishes certification from accreditation and explains why certificate details matter.
SunshinePro’s website refers to quality certifications, but buyers should request current documents before relying on those claims during supplier approval.
Perlakukan tanggapan ini sebagai tanda bahaya kualifikasi
| Tanggapan pemasok | Risiko yang diciptakan | Tindak lanjut yang tepat |
| "Kita dapat memenuhi toleransi" tanpa meninjau gambar lengkapnya | Fitur atau datum kritis mungkin terlewatkan | Minta tinjauan gambar yang ditandai dan metode inspeksi |
| Tidak ada perbedaan antara katalog dan spesifikasi khusus | Bagian yang dikutip mungkin tidak cocok dengan aplikasi | Memerlukan perbandingan spesifikasi yang tepat |
| Penolakan untuk mengungkapkan proses kritis outsourcing | Proses tersembunyi dan risiko pengiriman | Memerlukan kepemilikan proses dan informasi subkontraktor |
| Tidak ada revisi gambar terkontrol | Produksi dapat menggunakan file usang | Tentukan persyaratan kontrol revisi sebelum memesan |
| Tidak ada data dimensi sampel | Kemampuan tetap belum diverifikasi | Meminta contoh atau laporan artikel pertama |
| Penggantian material atau kekerasan tanpa persetujuan | Risiko fungsional dan pertukaran | Memerlukan persetujuan perubahan tertulis |
| Respons yang tidak jelas terhadap bagian yang tidak sesuai | Penundaan dan cacat berulang dapat terjadi | Minta prosedur penahanan dan tindakan korektif |
| Tidak ada kebijakan pemberitahuan perubahan | Pesanan berulang mungkin berbeda dari bagian yang disetujui | Menambahkan persyaratan kontrol perubahan kontrak |
One red flag does not always require immediate rejection. It should, namun, trigger a documented clarification or approval condition.
Kualifikasi pin batas kustom melalui sampel dan persetujuan artikel pertama
A promising quotation is not final proof of capability. For custom or function-critical limit pins, qualification should move through a controlled sample or first-article process.
- Freeze the drawing revision.
Confirm the exact drawing, model, spesifikasi, approved deviations, dan persyaratan inspeksi. - Review the proposed process route.
Confirm material, urutan pemesinan, perlakuan panas, penggilingan, pelapisan ulir, outsourced operations, dan inspeksi akhir. - Define the sample package.
State the sample quantity and required dimensional, material, kekerasan, pengobatan, or conformity records. - Use the intended production process.
The sample should represent the planned repeat-order method. A hand-finished prototype may not demonstrate production consistency. - Review actual measurement results.
Compare the report with every critical drawing characteristic. Do not accept a simple “passed inspection” statement when measured values were agreed. - Perform assembly or functional checks where needed.
Dimensional conformity may not reveal every seating, retensi, or stopping issue. - Resolve deviations formally.
Record rework, concessions, rejected characteristics, root causes, dan tindakan korektif. - Establish the approved baseline.
Preserve the approved drawing revision, material, process route, inspection plan, kemasan, and change-notification requirements for future orders.
A formal first-article package is project-dependent. Buyers should not assume that a supplier provides FAI, PPAP, capability studies, or control plans unless those deliverables are confirmed in the quotation.
Evaluate Repeat-Order, Pengganti, and Commercial Support
Technical approval is only part of manufacturer selection. Mold limit pins may later be reordered for maintenance, memperbaiki, pengganti, or additional molds. The supplier must therefore protect the approved configuration.
Evaluate:
- sample price and production price;
- setup charges and quotation exclusions;
- minimum order quantity;
- initial production lead time;
- repeat-order lead time;
- stocked versus made-to-order status;
- retained drawing revision;
- material, proses, or subcontractor change notification;
- batch identification and record retention;
- urgent replacement capability;
- nonconformance response;
- packaging and corrosion protection;
- thread and end-face protection;
- separation of similar part numbers;
- export packing and customs documents;
- agreed Incoterms;
- drawing confidentiality where required.
SunshinePro states that standard sizes can be supplied from stock and non-standard sizes can be customized. Its company profile also refers to flexible order quantities, technical support, and international cooperation. These points should be confirmed for the specific drawing, kuantitas, tujuan, and delivery requirement rather than treated as universal guarantees.
Bandingkan pemasok dengan gerbang lulus/gagal sebelum mencetak harga
A supplier scorecard is useful only after mandatory requirements are separated from preferences. A low quotation should not compensate for an unresolved material substitution, inadequate inspection method, uncontrolled drawing revision, or missing critical process.
Use a structure such as:
| Area evaluasi | Persyaratan wajib | Bukti | Status | Catatan risiko atau komersial |
| Ulasan gambar | Semua persyaratan penting diakui | Catatan gambar atau ulasan yang ditandai | Lulus/Gagal | Catatan pengecualian |
| Bahan | Nilai dan kondisi yang tepat dikonfirmasi | Sertifikat atau konfirmasi pemasok | Lulus/Gagal | Rekor pergantian pemain |
| Rute proses | Suitable machining, pengobatan, and finishing sequence | Ringkasan proses | Lulus/Gagal | Mengidentifikasi langkah-langkah outsourcing |
| Pengukuran | Metode yang cocok untuk setiap karakteristik kritis | Rencana inspeksi atau laporan sampel | Lulus/Gagal | Perhatikan batas pelaporan |
| Persetujuan sampel | Sampel dan catatan yang diperlukan diterima | FAI atau paket sampel yang disepakati | Lulus/Gagal | Catatan penyimpangan |
| Mengubah kontrol | Pemberitahuan pembeli sebelum perubahan penting | Kebijakan tertulis atau istilah kutipan | Lulus/Gagal | Menentukan rute persetujuan |
| Dukungan penggantian | Kondisi pesanan berulang dipahami | Konfirmasi waktu tunggu dan penyimpanan catatan | Skor | Pertimbangkan risiko waktu henti |
| Harga | Kutipan dibandingkan pada ruang lingkup yang sama | Kutipan komersial lengkap | Skor | Termasuk inspeksi dan pengemasan |
Only suppliers passing the mandatory gates should proceed to commercial scoring. The final comparison can then consider communication, responsiveness, evidence quality, replacement support, logistik, and total sourcing cost.
Total cost is broader than unit price. Pengerjaan ulang, delayed mold assembly, emergency freight, waktu istirahat, and requalification can exceed a small initial saving.
Bagaimana SunshinePro Menyatakan Limit Pin Menawarkan Peta ke Daftar Periksa
SunshinePro publishes several points relevant to an initial supplier review. Other items still need project-specific confirmation.
| Informasi yang dikonfirmasi situs web | Konfirmasi selama RFQ |
| Penawaran produk pin batas cetakan hidup | Kesesuaian yang tepat untuk fungsi dan gambar pembeli |
| Ukuran standar dijelaskan sebagai tersedia dari stok | Stok saat ini untuk spesifikasi yang diperlukan |
| Kustomisasi ukuran non-standar | Kelayakan geometri dan toleransi yang tepat |
| S45C terdaftar untuk produk yang ditampilkan | Ketersediaan dan kesesuaian bahan yang dibutuhkan |
| Displayed diameter, panjang, and hardness values | Contractual dimensions, toleransi, and hardness for the custom order |
| Fitur berulir yang disebutkan | Standar benang dan metode inspeksi yang berlaku |
| Penggilingan presisi diameter luar dijelaskan | Rute penggilingan yang tepat dan hasil khusus gambar yang dapat dicapai |
| Perlakuan panas vakum dijelaskan | Process ownership, specification, rekaman, and distortion control |
| Initial, in-process, and final inspection stated | Characteristics checked, instruments used, and reports supplied |
| Alur kerja tinjauan gambar dan kutipan | Sample package, waktu tunggu, MOQ, change control, and repeat-order terms |
The company’s public information can support the first screening stage. Final manufacturer approval should still be based on the released drawing, written quotation, agreed process, requested evidence, and sample results.
Daftar Periksa Pemilihan Produsen Pra-RFQ Akhir
Before approving a supplier or sending a production order, mengonfirmasi bahwa:
- the limit pin’s function is clearly defined;
- the correct part type has been identified;
- the standard or custom sourcing path is decided;
- the drawing revision is controlled;
- material, kekerasan, geometri, menyelesaikan, and threads are specified;
- critical-to-quality characteristics are identified;
- the manufacturer has explained the process route;
- outsourced processes are disclosed;
- the inspection method suits each critical requirement;
- required reports and certificates are agreed;
- sample or first-article approval is defined;
- substitutions require written approval;
- repeat-order and change-control expectations are documented;
- packaging protects the part during international shipment;
- quotations are compared on the same technical and quality scope;
- unresolved red flags are closed before production.
Buyers with a completed drawing, contoh, quantity requirement, and inspection expectations can hubungi SunshinePro for a feasibility review and quotation. The request should ask for confirmation of the proposed material, rute manufaktur, inspection evidence, sample plan, and commercial terms—not only a unit price.
Bagikan:



Ditulis oleh Sunshine
di Sunshine, Kami adalah produsen dan pemasok profesional komponen cetakan presisi, menawarkan berbagai produk untuk aplikasi stamping dan cetakan injeksi. Fokus utama kami adalah mencetak cetakan, pin dan lengan ejector, serta tiang panduan dan bushing. Dengan pemesinan CNC canggih, kontrol kualitas ketat, dan kemampuan produksi yang kuat, kami memastikan keandalan, suku cadang presisi tinggi, bersama dengan komponen standar yang tersedia untuk pasokan global yang cepat dan efisien.
BERITA
DAPATKAN LAYANAN
Dengan suku cadang berkualitas untuk memenuhi setiap anggaran dan staf ramah yang terlatih untuk membuat kunjungan Anda menjadi informatif dan tanpa repot.
