



Panduan Cetakan Injeksi: Komponen, Jenis-jenis, dan Cara Kerjanya
Injection mold systems are precision tools used to shape molten plastic into repeatable parts during injection molding production. A typical injection mold includes the cavity, core, runner system, saluran pendingin, and ejector components. Mold type, pemilihan material, and cooling design directly affect part quality, production speed, tooling cost, dan masa pakai jamur.
An injection mold determines how a plastic part looks, fits, and performs. Even small tooling decisions can affect cycle time, defect rates, and long-term production cost. This guide explains how injection molds work, what components matter most, and how manufacturers choose the right mold setup for different production goals.
What is an injection mold?
An injection mold is a precision tooling system used to shape molten plastic into repeatable parts during injection molding. The mold controls the part’s final shape, dimensi, finishing permukaan, dan konsistensi produksi.
An injection mold is the custom-built tool installed inside an injection molding machine. Molten plastic flows into the mold cavity under pressure, cools into shape, and then ejects as a finished part. The same mold can produce thousands or even millions of identical components when maintained correctly.
The mold itself contains several engineered systems that control material flow, pendinginan, penyelarasan, dan sebagian rilis. That’s why tooling quality has such a strong impact on production efficiency and defect prevention.
If you’re new to the manufacturing process, ini Panduan Cetakan Injeksi Plastik explains the broader molding workflow and machine operation in more detail.
For a technical overview of molding fundamentals, the Ikhtisar cetakan injeksi Global TWI provides a useful industry reference.
How does an injection mold work during production?
Injection molds work by receiving molten plastic under pressure, cooling the material inside a precision cavity, and ejecting the finished part after solidification. The process repeats rapidly for high-volume production.
The process starts with plastic pellets melting inside the injection molding machine barrel. The machine pushes the molten plastic into the mold cavity through a runner and gate system. Once the cavity fills, the mold holds pressure while the material cools and hardens.
Cooling time matters more than many buyers expect. A poorly designed cooling layout can slow production dramatically and increase warping or shrinkage issues. In high-volume manufacturing, even a few seconds added to cycle time can affect overall production cost.
Fase injeksi
Selama injeksi, the mold must stay tightly clamped to handle pressure. The cavity and core shape the plastic into its final geometry. Gates control how material enters the part, while runners distribute material through the mold.
A consumer electronics housing with thin walls, misalnya, often requires balanced flow paths to prevent cosmetic marks and incomplete filling.
Fase pendinginan dan ejeksi
Setelah pendinginan, ejector pins push the part out of the mold. The mold then closes again, and the cycle repeats. Efficient cooling design helps reduce downtime and improve production speed.
Ini Panduan kemampuan cetakan Protolabs explains how moldability and cooling design affect manufacturing performance.
For a broader explanation of production flow, lihat ini Panduan proses pencetakan injeksi.
What are the main components of an injection mold?
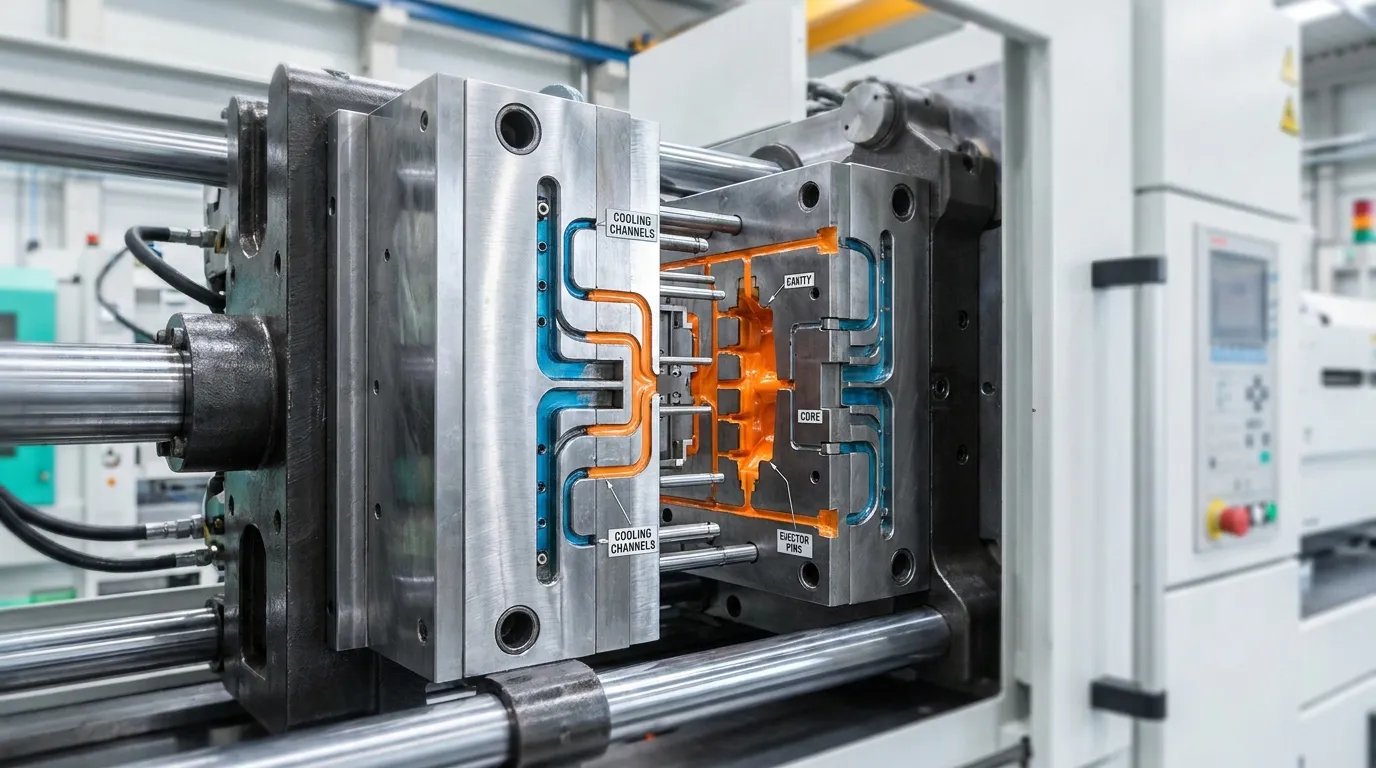
Injection mold components work together to control plastic flow, pendinginan, penyelarasan, and part ejection. Core systems include the cavity, runner system, Ejector, saluran pendingin, and guide mechanisms.
Every injection mold includes several mechanical systems that must work together with tight precision. If one area fails, the entire molding process can suffer from defects, waktu istirahat, or inconsistent dimensions.
| Komponen | Fungsi | Mengapa Itu Penting |
|---|---|---|
| Rongga | Membentuk bentuk luar bagian | Mengontrol dimensi dan permukaan akhir |
| Inti | Membuat fitur internal | Memengaruhi kecocokan dan geometri struktural |
| Sistem pelari | Mengarahkan aliran plastik cair | Berdampak pada pengisian saldo |
| Gerbang | Titik masuk ke dalam rongga | Memengaruhi garis dan tanda las |
| Saluran pendingin | Menghilangkan panas dari cetakan | Mengurangi waktu siklus |
| Pin ejektor | Dorong bagian jadi keluar | Mencegah lengket dan kerusakan |
| Pin panduan | Sejajarkan bagian cetakan | Menjaga presisi selama penjepitan |
Cooling channels often receive less attention than cavities or gates, but they directly affect production efficiency. A redesigned cooling layout can shorten cycle time significantly during high-volume production runs.
Misalnya, a medical component with tight tolerances may require advanced cooling paths and hardened steel inserts to maintain dimensional stability across long production runs.
Ini Gambaran Umum Komponen Cetakan provides a deeper look at individual tooling systems and their engineering roles.
For additional mold construction details, the Referensi Konstruksi Cetakan Injeksi offers a useful technical resource.
What are the different types of injection molds?
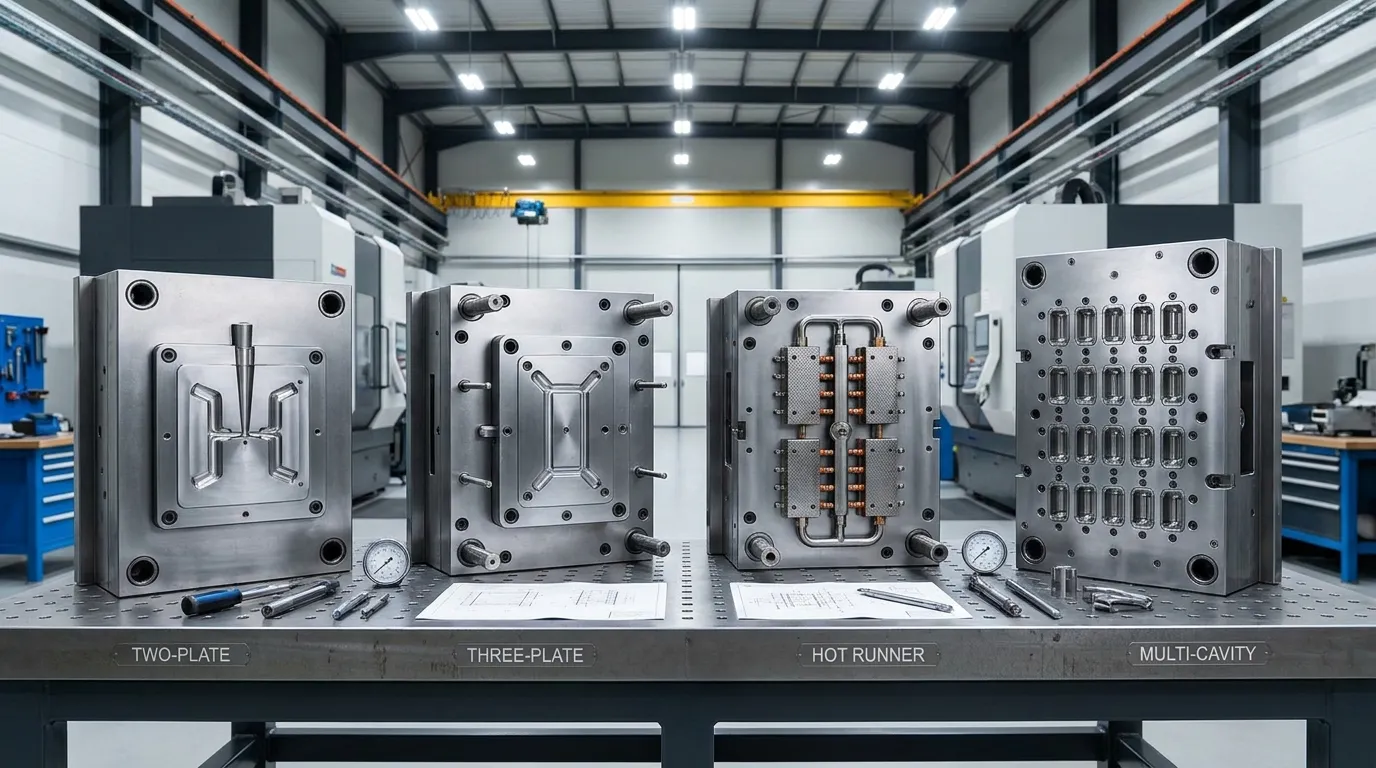
Different injection mold types are designed for different production needs. Simpler molds reduce tooling cost, while advanced systems like hot runner molds improve cycle efficiency and reduce material waste.
Manufacturers select mold types based on production volume, part complexity, gating requirements, and budget. Some molds focus on lower tooling cost, while others prioritize faster production and reduced scrap.
Cetakan dua pelat vs tiga pelat
A two-plate mold uses a single parting line and simpler runner system. It works well for many standard plastic parts and usually costs less to manufacture.
A three-plate mold adds an extra plate that allows more flexible gate placement. This helps with complex geometries and automatic runner separation, but it also increases tooling complexity and maintenance requirements.
| Jenis Cetakan | Terbaik Untuk | Keuntungan utama | Kelemahan Utama |
|---|---|---|---|
| Cetakan dua pelat | Suku cadang produksi standar | Biaya perkakas yang lebih rendah | Penempatan gerbang terbatas |
| Cetakan tiga pelat | Tata letak gerbang yang kompleks | Fleksibilitas gerbang yang lebih baik | Pemeliharaan yang lebih tinggi |
| Cetakan pelari panas | Produksi volume tinggi | Lebih sedikit limbah material | Biaya di muka yang lebih tinggi |
| Cetakan multi-rongga | Produksi besar | Output per siklus yang lebih tinggi | Lebih menyeimbangkan kompleksitas |
Hot runner molds are not always the best choice. They improve material efficiency, but simpler cold runner systems are often safer for lower production volumes or products with frequent material changes.
A low-volume prototype project, for instance, may benefit more from a simpler tooling design with lower upfront investment.
Ini Panduan Aplikasi Cetakan Industri explains how different mold setups fit various industries and product categories.
Which materials are used to make injection molds?
Steel molds are preferred for long production runs and tight tolerances, while aluminum molds reduce tooling cost and speed up prototyping. Material selection depends on production volume, part complexity, and expected mold lifespan.
Tool steel is the most common mold material for long-term production. Hardened steel handles high injection pressure, bahan abrasif, and repeated cycles better than softer metals. It’s commonly used for automotive, medis, and industrial production programs.
Aluminum molds are lighter and easier to machine. That makes them useful for prototyping, perkakas jembatan, and shorter production runs where speed matters more than maximum lifespan.
| Bahan | Penggunaan Terbaik | Kekuatan | Batasan |
|---|---|---|---|
| Baja yang dikeraskan | Produksi yang panjang | Daya tahan tinggi | Biaya lebih tinggi |
| Baja pra-pengerasan | Perkakas volume sedang | Pemesinan yang lebih mudah | Umur yang lebih pendek |
| Aluminium | Prototipe dan eksekusi volume rendah | Lead time lebih cepat | Ketahanan aus yang lebih rendah |
Aluminum molds reduce lead time and tooling cost, but steel molds are usually the better long-term investment for high-volume production. A medical connector produced in large quantities may justify hardened steel tooling because dimensional consistency matters over millions of cycles.
How long does injection mold production take?
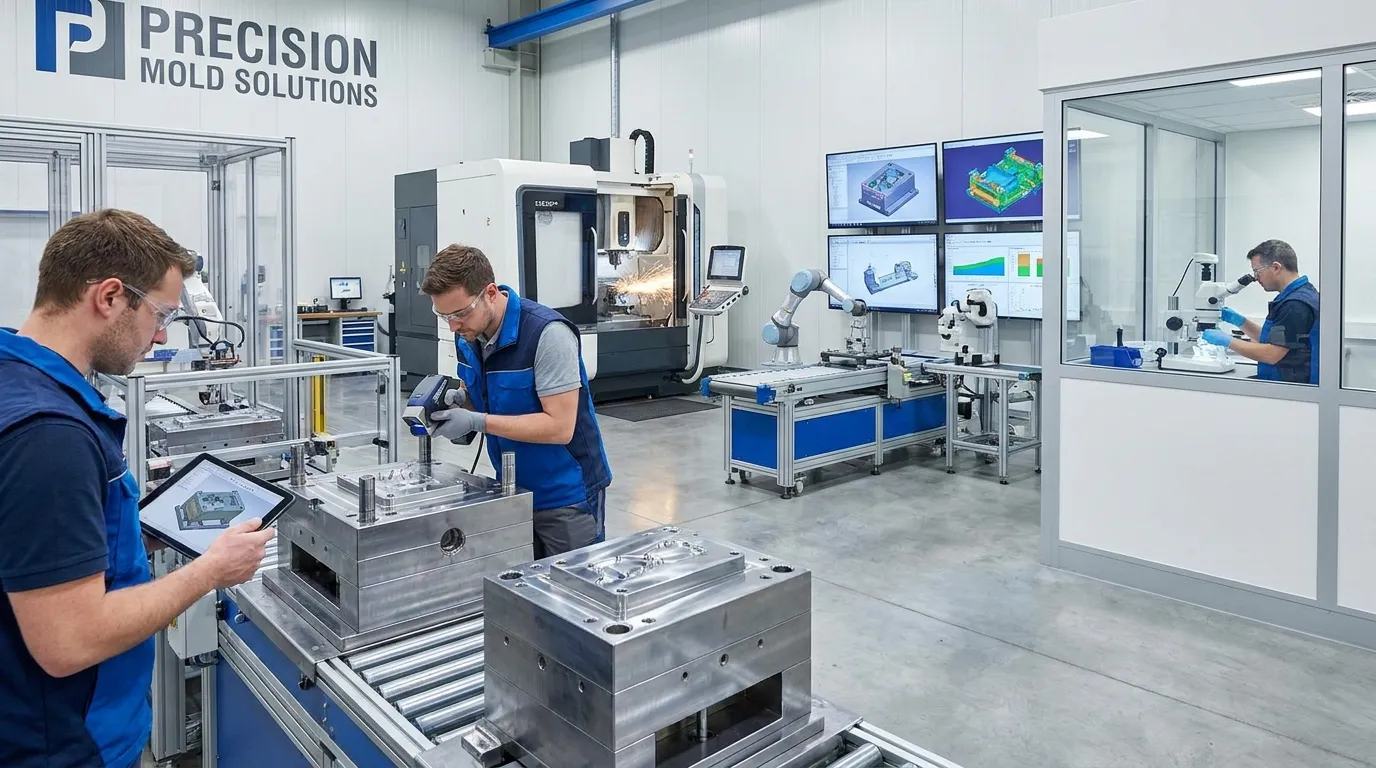
Injection mold lead times commonly range from several weeks to several months depending on mold complexity, hitungan rongga, revisi alat, dan persyaratan validasi.
Lead time depends on more than machining speed. Mold design reviews, material sourcing, pengambilan sampel, and validation testing all affect delivery schedules. Complex multi-cavity molds naturally take longer because they require tighter balancing and additional machining steps.
A simple prototype mold may move from design approval to sampling quickly. A multi-cavity production tool for consumer electronics can take much longer due to cosmetic requirements and repeated validation testing.
Faktor-faktor yang menunda pengiriman cetakan
- Revisi desain setelah pemotongan baja
- Penundaan sumber baja perkakas khusus
- Permintaan pengambilan sampel tambahan
- Aliran cetakan atau koreksi pendinginan
- Penundaan pengiriman dan bea cukai internasional
Faster tooling timelines are not always a positive sign. Aggressive schedules can reduce testing time and increase production issues later.
| Tahap Produksi | Fokus Khas |
|---|---|
| Persetujuan desain | Tinjauan DFM dan validasi suku cadang |
| Pemesinan CNC | Pembuatan basis cetakan dan rongga |
| Perakitan | Memasang komponen dan sistem |
| Pengambilan sampel | Memproduksi suku cadang uji awal |
| Validasi | Pemeriksaan dimensi dan kosmetik |
Ini Panduan waktu tunggu EvokPoly explains how tooling complexity affects scheduling. Itu Artikel tren manufaktur fiktif also highlights how automation and digital validation are changing mold production workflows.
What problems can affect injection molds?
Injection molds can develop production problems from wear, cooling imbalance, alignment issues, or poor maintenance. Many defects start small and become expensive only after production volumes increase.
Flash happens when molten plastic escapes along the mold parting line. Short shots occur when the cavity does not fill completely. Uneven cooling can also create warping, bekas tenggelam, or dimensional instability.
Dasar-dasar pemeliharaan cetakan
Regular maintenance helps prevent unexpected downtime and part inconsistency. Most production teams monitor wear surfaces, saluran pendingin, sistem ejector, and alignment components during scheduled inspections.
A high-volume packaging mold, misalnya, may require more frequent cleaning because resin buildup can affect gate performance and filling consistency.
Daftar periksa masalah jamur umum
- Berkedip di sekitar tepi bagian
- Bidikan pendek atau pengisian yang tidak lengkap
- Ketidakseimbangan pendinginan
- Pin ejektor aus
- Penyimpangan penyelarasan cetakan
- Penyumbatan gerbang
- Goresan atau tanda permukaan
Ini Panduan Komponen Cetakan Presisi explains how individual tooling systems influence mold precision and maintenance planning.
How do manufacturers choose the right injection mold design?
Choosing the right mold design depends on production volume, pemilihan material, part geometry, and long-term cost goals. The best tooling setup is usually the one that balances reliability, cycle efficiency, and maintenance needs.
A low-volume consumer product may use aluminum tooling to reduce launch cost and shorten development time. A medical device component with strict tolerances often requires hardened steel tooling and tighter validation procedures.
Tabel perbandingan jenis cetakan injeksi
| Kebutuhan Produksi | Pengaturan Cetakan yang Direkomendasikan | Mengapa Cocok |
|---|---|---|
| Bagian prototipe | Cetakan aluminium | Perputaran lebih cepat |
| Produksi menengah | Cetakan baja dua pelat | Biaya dan daya tahan yang seimbang |
| Kemasan volume tinggi | Cetakan multi-rongga pelari panas | Efisiensi siklus lebih cepat |
| Bagian medis toleransi ketat | Cetakan baja yang dikeraskan | Stabilitas dimensi yang lebih baik |
| Perumahan elektronik kosmetik | Sistem pelari seimbang multi-rongga | Peningkatan konsistensi visual |
Part geometry also changes tooling strategy. Thin-wall electronics housings often require balanced runner layouts and advanced cooling control. Deep ribs, memotong, or textured surfaces may increase tooling complexity and maintenance requirements.
Manufacturers also evaluate long-term operating cost. A cheaper mold can become expensive later if cycle times stay slow or maintenance needs increase.
Ini Panduan Aplikasi Cetakan Injeksi shows how tooling decisions vary across industries and product categories.
Apa yang Harus Dilakukan Selanjutnya
An injection mold affects far more than part shape. It influences production speed, maintenance needs, defect rates, and long-term manufacturing cost. That’s why mold design decisions should match the product’s production goals instead of focusing only on upfront tooling price.
If you're comparing mold options, start by defining production volume, persyaratan material, and quality expectations first. Then review cooling strategy, cavity layout, and mold material selection with your supplier. A well-designed injection mold usually saves far more money during production than it costs during tooling development.
Pertanyaan yang Sering Diajukan
What is an injection mold used for?
An injection mold is used to manufacture repeatable plastic parts by shaping molten material inside a precision cavity. It’s widely used for automotive, elektronika, medis, and consumer products that require consistent dimensions and high production volume.
What are the main parts of an injection mold?
The main parts include the cavity, core, runner system, gate, saluran pendingin, Sistem ejektor, and guide components. Each system controls how plastic flows, mendinginkan, aligns, and releases during production.
What is the difference between a two-plate and three-plate mold?
A two-plate mold uses one parting line and a simpler runner system, while a three-plate mold adds a separate runner plate for flexible gate placement. Three-plate molds improve gating control but increase tooling complexity and maintenance.
Berapa lama waktu yang dibutuhkan untuk membuat cetakan injeksi?
Injection mold production can take several weeks to several months depending on complexity, hitungan rongga, testing requirements, and design revisions. Large production tools usually require longer validation and sampling stages.
Why are injection molds expensive?
Injection molds require precision machining, engineered cooling systems, hardened materials, and detailed testing. Higher cavity counts, toleransi ketat, and complex part geometries increase tooling cost significantly.
How many parts can one injection mold produce?
Mold lifespan depends on tooling material, maintenance quality, dan kondisi produksi. Hardened steel molds can often produce hundreds of thousands or even millions of cycles when maintained properly.
Bagikan:



Ditulis oleh Sunshine
di Sunshine, Kami adalah produsen dan pemasok profesional komponen cetakan presisi, menawarkan berbagai produk untuk aplikasi stamping dan cetakan injeksi. Fokus utama kami adalah mencetak cetakan, pin dan lengan ejector, serta tiang panduan dan bushing. Dengan pemesinan CNC canggih, kontrol kualitas ketat, dan kemampuan produksi yang kuat, kami memastikan keandalan, suku cadang presisi tinggi, bersama dengan komponen standar yang tersedia untuk pasokan global yang cepat dan efisien.
BERITA
DAPATKAN LAYANAN
Dengan suku cadang berkualitas untuk memenuhi setiap anggaran dan staf ramah yang terlatih untuk membuat kunjungan Anda menjadi informatif dan tanpa repot.
